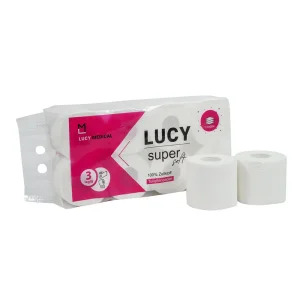
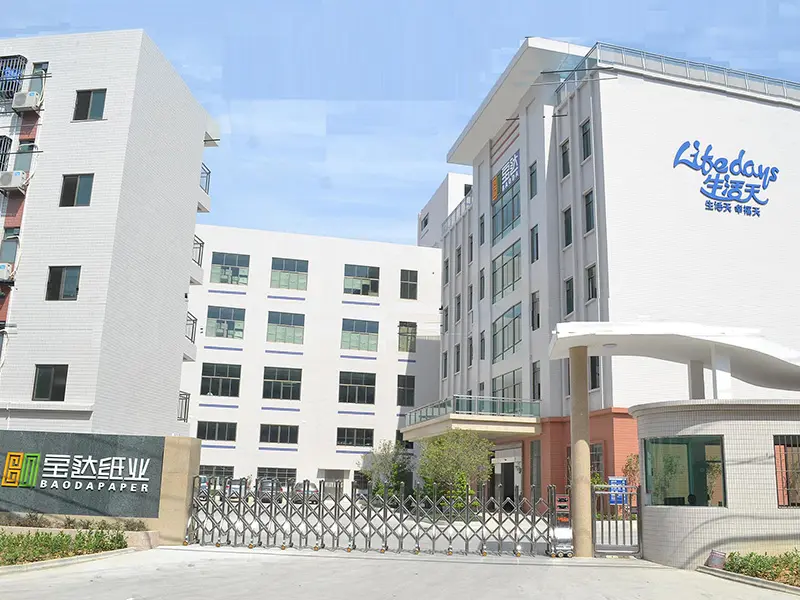
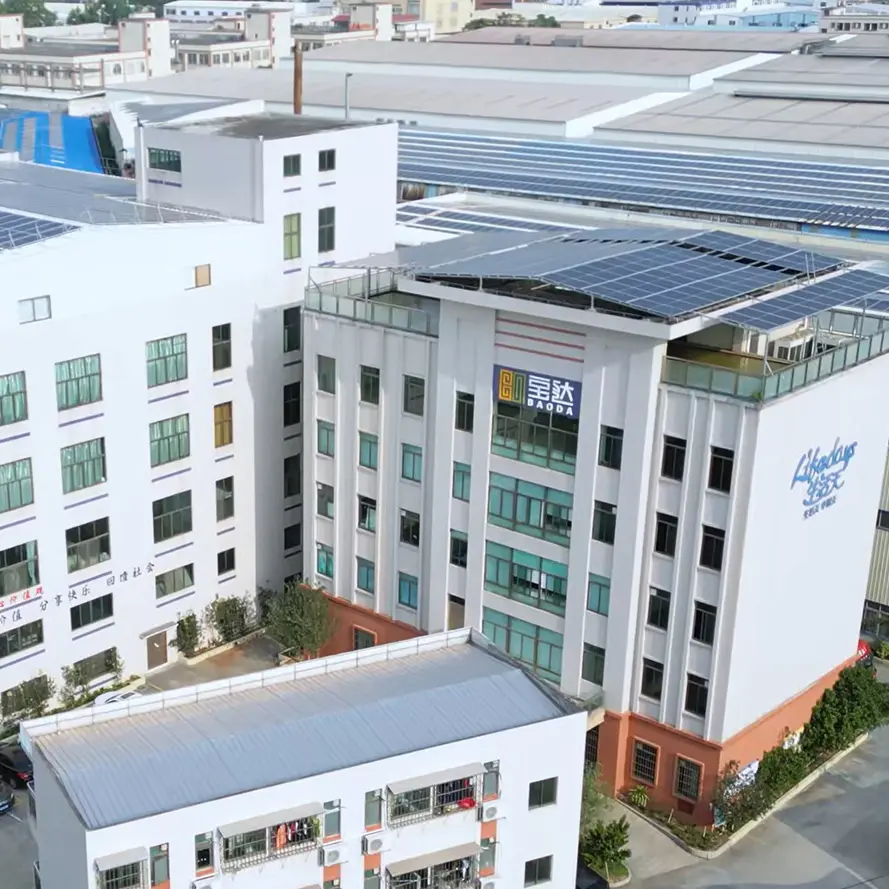
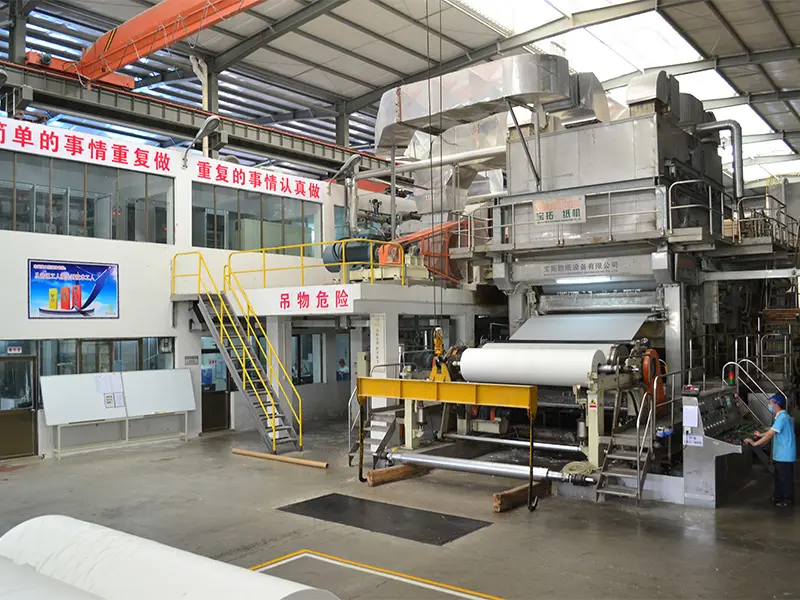
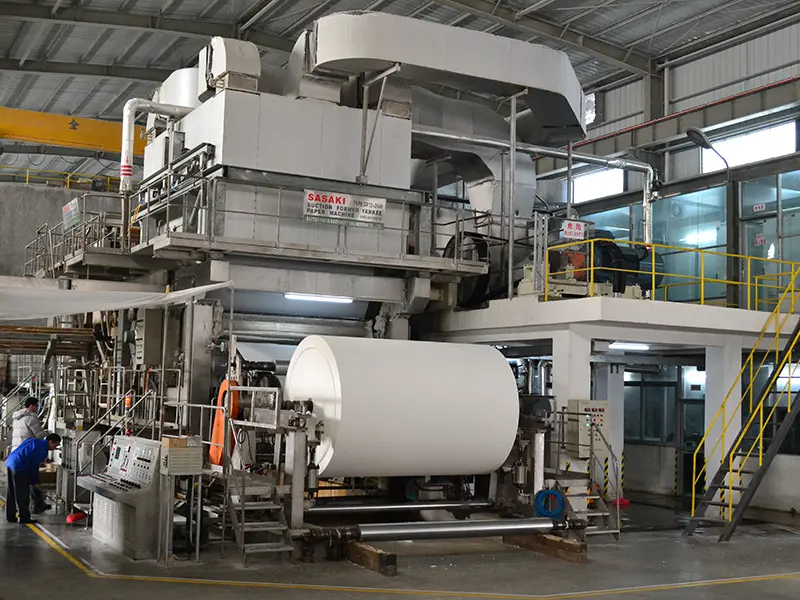
For over 27 remarkable years, since our inception in 1998, Baoda Paper Co., Ltd. has stood as an unwavering cornerstone of China's tissue paper industry, evolving from a domestic manufacturer into a globally recognized force. We have meticulously built our legacy on a formidable foundation of advanced manufacturing excellence and an unwavering commitment to quality. Our modern, sprawling complex, exceeding 20,000 square meters, is a testament to this commitment.
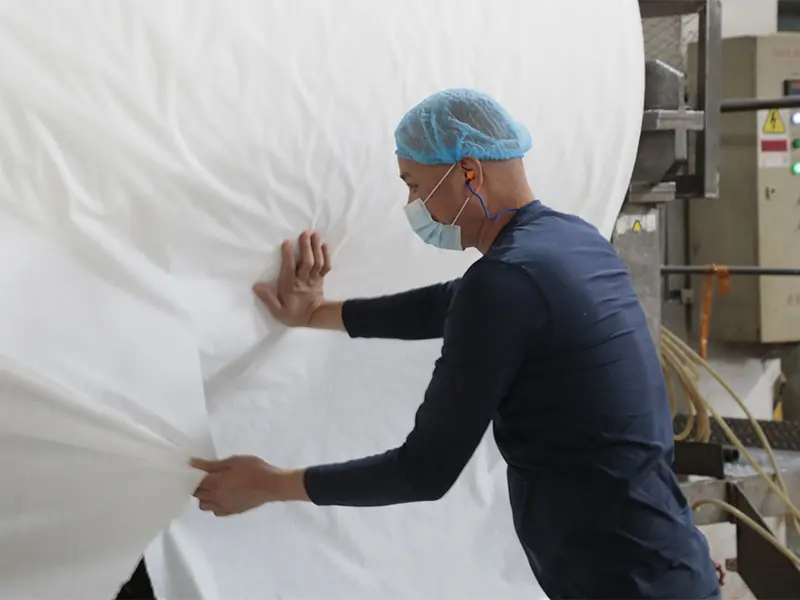
Within its walls, we house state-of-the-art, imported high-speed paper machines and sophisticated automated processing lines. This powerful infrastructure is the engine behind our impressive annual production capacity of over 30,000 tons, enabling us to meet large-scale demands without compromising on the consistent quality that defines the Baoda name. Our integrated solutions bridge the gap between material raw processing and direct retail distributions.
Modern kitchen wet tissues are not merely damp cloths; they represent a precise combination of substrate physics and organic chemistry designed to address heavy organic greases (lipids, proteins, starches) common to high-heat cooking environments. Choosing the correct formulation determines cleanability, surface protection, and skin safety.
We utilize Alkyl Polyglycosides (APG) derived from renewable plant materials. These non-ionic surfactants provide exceptional wetting, dispersing, and surface tension reduction, breaking down stubborn polymerised cooking oils without leaving toxic residues.
Unlike parallel-laid fibers that tear easily under pressure, our cross-lapped non-woven substrates offer isotropic tensile strength. This ensures high durability during vigorous scrubbing on abrasive cast-iron and stainless steel surfaces.
Our formulation incorporates quick-evaporating deionized water (EDI purified to <10 microsiemens/cm) and mild solvents. This leaves glass, ceramic hobs, and marble surfaces completely free of streaks and film buildup.
| Substrate Material Type | Composition (Polyester / Viscose) | Tensile Strength (MD/CD) | Absorbency Capacity | Biodegradability Rate | Primary Industrial Use Case |
|---|---|---|---|---|---|
| Virgin PET/Viscose Blend | 70% Polyester / 30% Viscose | High (>45 N/5cm) | 450% by weight | Partial (Slow degradation) | Commercial kitchens & heavy duty degreasing |
| Spunlace Woodpulp/PP | 50% Pulp / 50% Polypropylene | Medium (30-35 N/5cm) | 600% by weight | Moderate (Degradable core) | Single-use sanitizing wipes & oil absorption |
| Eco-Bamboo Fiber | 100% Bamboo Viscose | Excellent (>50 N/5cm) | 550% by weight | 100% Biodegradable (90 days) | Consumer premium eco-friendly markets |
| Airlaid Embossed Paper | 100% Fluff Wood Pulp | Lower (Dry use primary) | 800% by weight | 100% Compostable | Light duty wiping & immediate grease absorption |
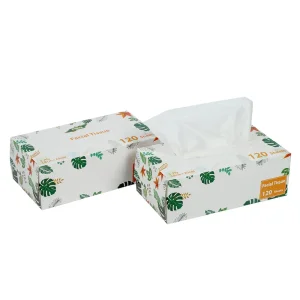
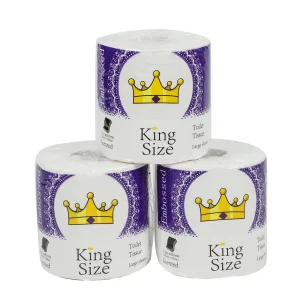
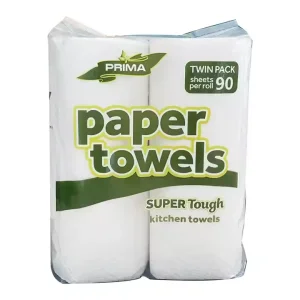
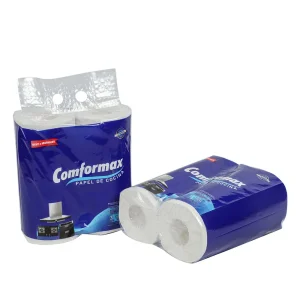
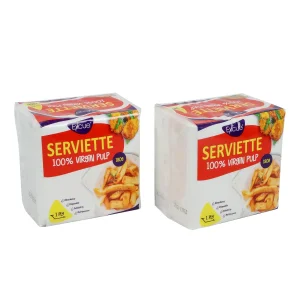
Our comprehensive and curated product portfolio is designed to provide complete one-stop solutions for diverse market needs. We offer an extensive range of products, from essential household items like premium toilet rolls, versatile kitchen towels, and soft facial tissues to convenient and hygienic pocket tissue packs for on-the-go use.
Understanding the diverse paths to market success, our business model is both robust and flexible. While we proudly market three successful self-owned brands, we are also a premier partner for clients seeking to build their own product lines. We specialize in tailored ODM (Original Design Manufacturing), OEM (Original Equipment Manufacturing), and OBM (Original Brand Manufacturing) services, working collaboratively to bring our clients' unique visions and brand identities to life with precision and expertise.
Backed by our 27 years of manufacturing experience, we maintain direct control over our entire supply chain. This means lower lead times, stable pricing structures, and customizable product features from dimensions and GSM (grams per square meter) to active cosmetic ingredients.
Our scale and operational efficiency allow us to support massive global retail channels with short lead times and unwavering product consistency.
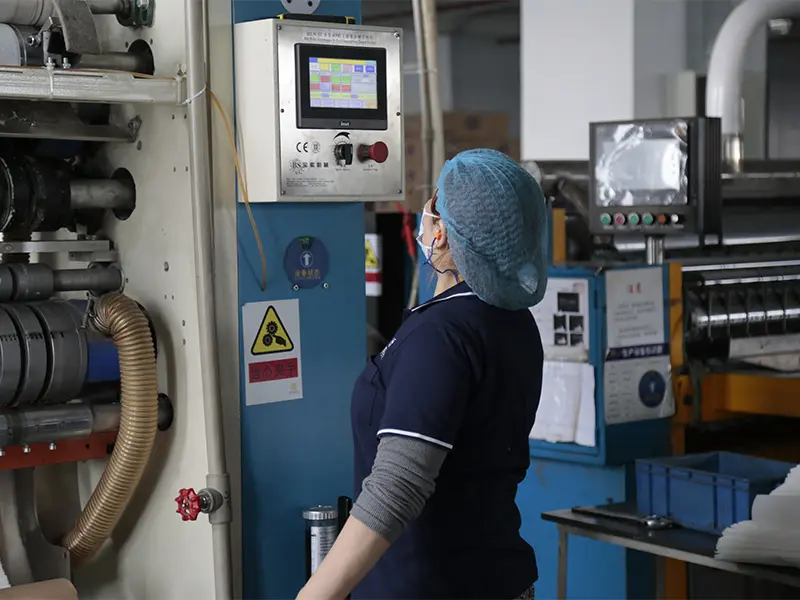
In the highly competitive kitchen wiping products market, cost efficiency and supply stability are paramount. At Baoda, we have transitioned our factory processes to follow the Factory 4.0 paradigm, using IoT sensors, automatic material dispensing, and enclosed ultra-clean packaging lines to deliver reliable volume production.
Raw municipal water is processed through quartz sand, activated carbon filters, dual-stage reverse osmosis (RO), and continuous Electrodeionization (EDI) systems to achieve pharmaceutical-grade purity.
Spunlace parent rolls are slit and folded via high-precision mechanical guides. Formulations are dosed online using smart volumetric pumps that ensure a uniform liquid saturation ratio across every single wipe.
Wipes are automatically wrapped with high-barrier plastic films and fitted with injection-molded flip lids. Flow-wrappers seal the packages under positive pressure, preventing micro-contamination.
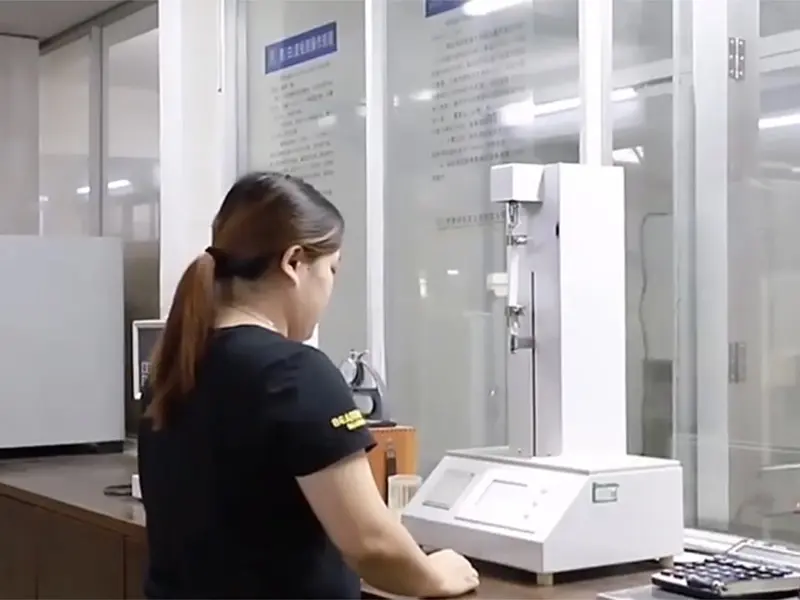
Metal detectors and automatic optical inspection (AOI) cameras check every package for sealing integrity, proper alignment, and contamination before cartoning and palletizing.
Baoda Paper provides tailor-made solutions across various commercial and domestic market segments. We design our products to handle different types of grime, frequency of use, and local regulatory requirements.
High-shelf-appeal packaging, customized fragrances (citrus, lavender, tea tree), and dermatologically tested formulations. Ideal for major supermarkets looking to build reliable, high-margin private label programs.
Extra-large sheet sizes, high gsm substrates, and sanitizing formulations compliant with food safety regulations. These wipes help professional kitchen staff maintain hygiene standards quickly between shifts.
Formulations with high concentrations of grease solvents and scrubby textured substrates. Built to tackle heavy lubricants, automotive grease, and adhesives while protecting workers' skin.
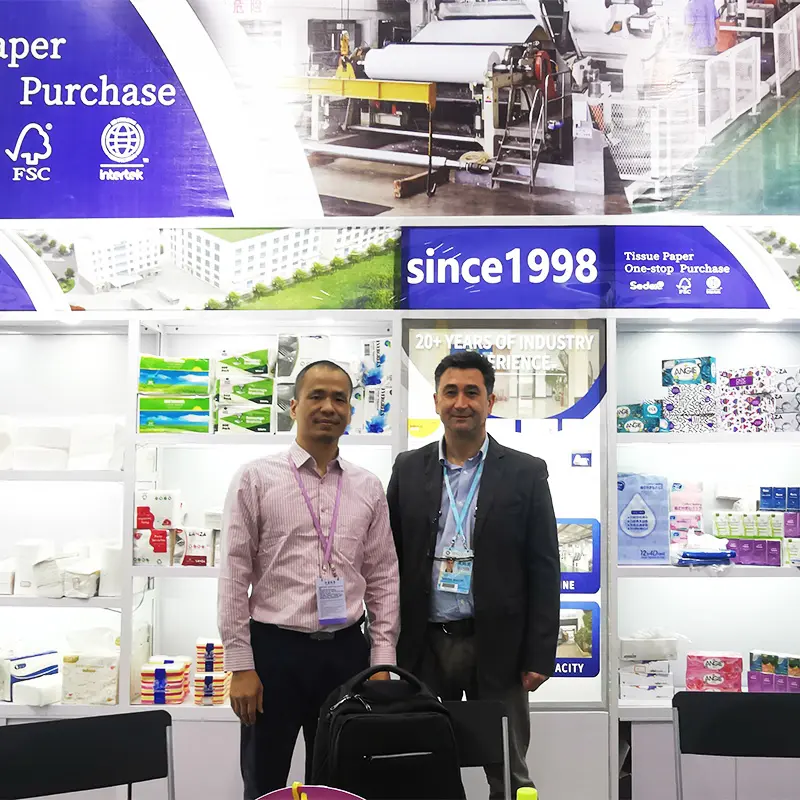
Our long-term focus has earned us the trust of a vast network of over 10,000 global leaders in retail and distribution, including renowned brands such as Walmart and Watsons.
Our high-quality products and reliable services have enabled us to build a robust international distribution network spanning more than 60 countries across the Americas, Europe, Asia, and Australia, with a strong presence in key markets like the United States and Australia. We maintain strict control over raw material tracing, chemical formulations, and logistics pathways, ensuring peace of mind for our clients.
Entering international retail and professional channels requires strict compliance with diverse regional chemical, mechanical, and safety standards. Baoda Paper manages the testing and certification processes to ensure smooth entry into these markets.
Compliance with FDA cosmetics guidelines, EPA registrations for antimicrobial agents, and Prop 65 requirements. Packaging options include multi-pack canisters and flat-pack refills for club stores.
Full compliance with REACH chemical registration requirements and EN 1276 testing for bactericidal activity. We also offer plastic-free, FSC-certified compostable substrate options to meet EU single-use plastic regulations.
Custom packaging configurations, multi-lingual labeling, and formulations optimized for high-humidity climates. Includes soft-packs with resealable tape closures designed for space-conscious households.
Full support for OEM, ODM, and OBM specifications. We accommodate custom formulations, emboss patterns, sheet sizes, pack counts, and private label branding to match your target demographics.
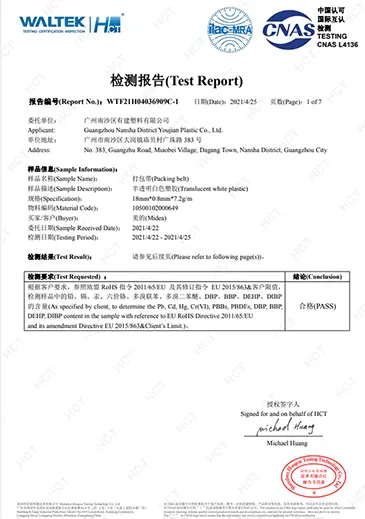
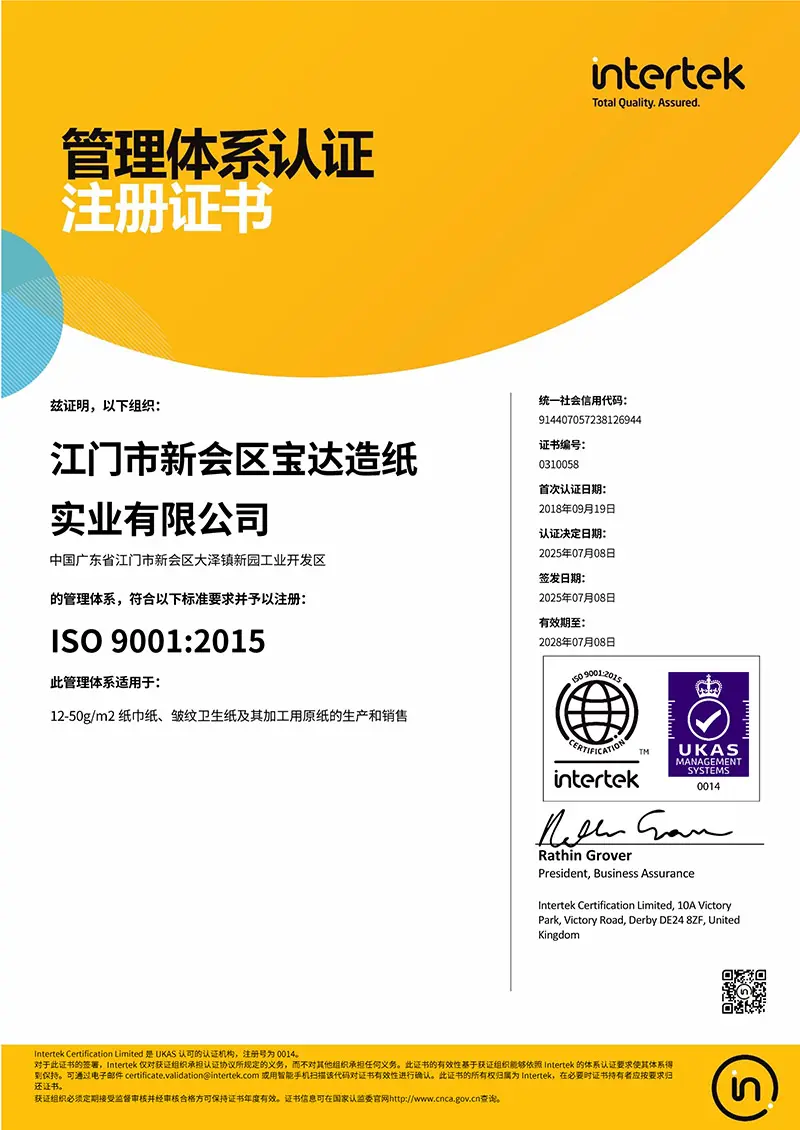
ISO 9001 Certified
GMPC Compliant
FSC Forestry Chain
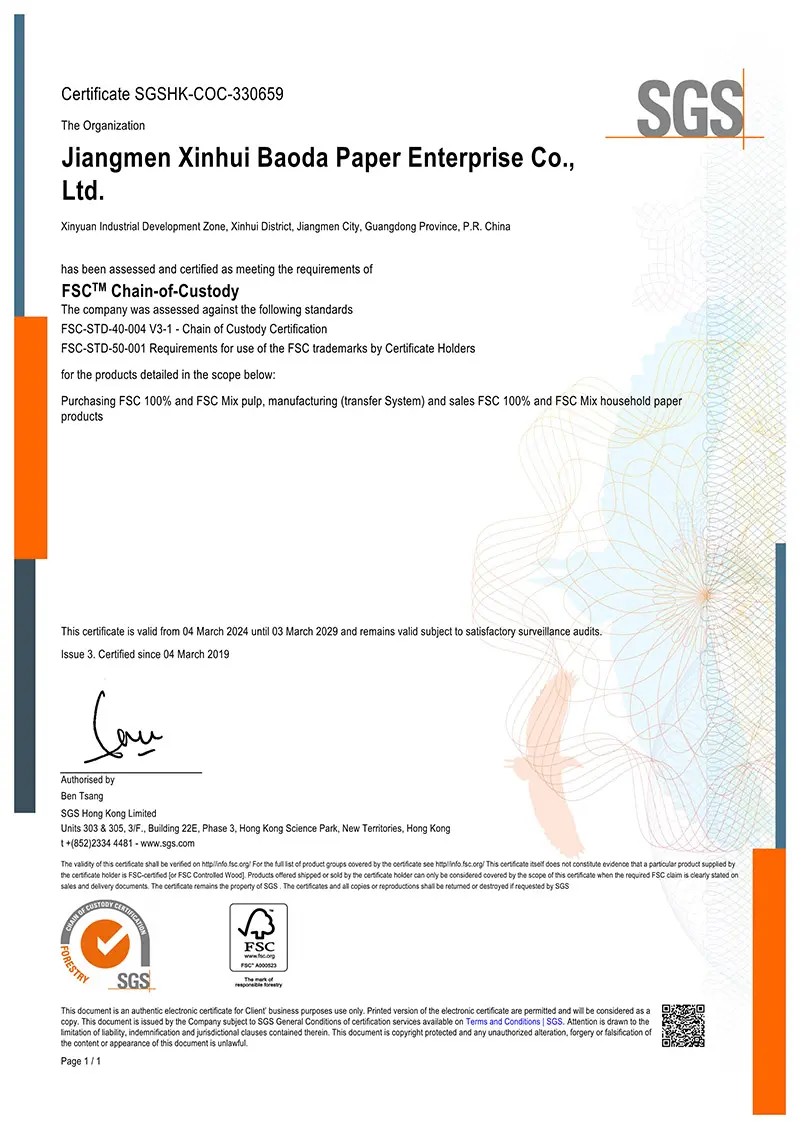
REACH Chemicals Safe
FDA Compliant Quality
The global cleaning products sector is shifting toward sustainability, high formulation efficiency, and skin-friendly chemistry. Our R&D team is focused on bringing these key innovations to our production lines over the coming years:
We are expanding our lines of woodpulp-lyocell and bamboo-viscose blended spunlace non-woven materials. These plant-derived fibers biodegrade completely in soil within 90 days, eliminating microplastics without sacrificing wet strength.
Our lab is testing lipase-enriched formulations that target lipid molecules. These enzymes continuously break down grease film on surfaces even after wiping, reducing dirt buildup and static dust collection over time.
To reduce plastic waste, we are transitioning our flow-wrap packaging to use mono-material polypropylene films (MDO-PE). These films are fully recyclable while maintaining the moisture barrier needed for a 2-year shelf life.
We are replacing traditional synthetic chemical preservatives with food-grade organic acids and botanical extracts. This provides antimicrobial protection against mold and bacteria in open packs while remaining safe for food-contact surfaces.
Essential information for B2B procurement managers, supply chain directors, and retail category buyers planning their kitchen tissue imports.
 BAODA PAPER