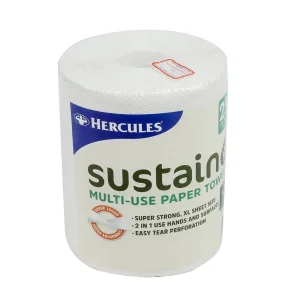
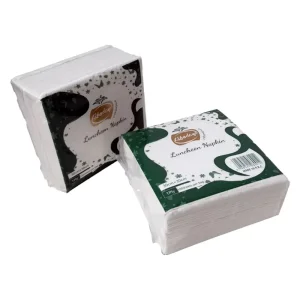
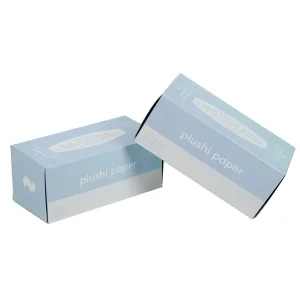
Explore our premium grade pulp solutions manufactured directly from state-of-the-art facilities, engineered to fulfill demanding international B2B and retail requirements.
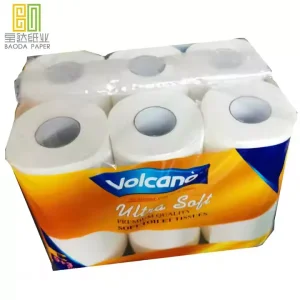
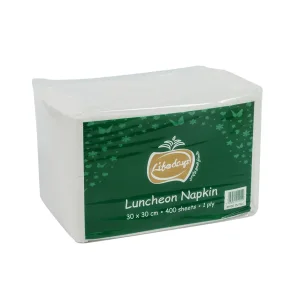
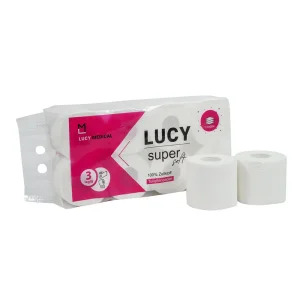
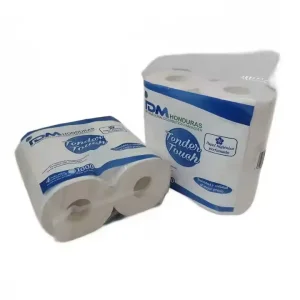
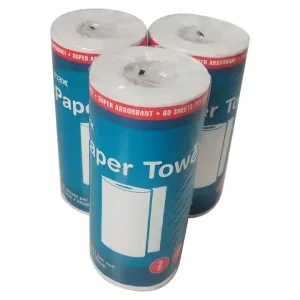
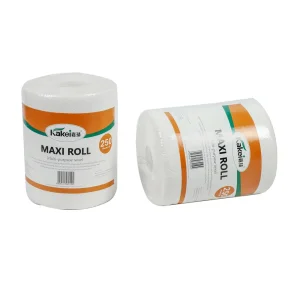
Founded in 1998, Baoda Paper Co., Ltd. has spent over 27 remarkable years evolving from a local manufacturer into a globally recognized force in the tissue paper sector. Headquartered in a modern manufacturing complex spanning over 20,000 square meters, we deploy imported high-speed paper machines alongside automated converting lines. This robust mechanical framework translates directly into a robust annual production capacity exceeding 30,000 tons of premium tissue products.
As a key OEM, ODM, and OBM production partner to multi-national operations, our commercial footprint spans over 60 countries throughout the Americas, Europe, Asia, and Australia. We are trusted by industry behemoths, including global giants such as Walmart and Watsons, demonstrating our capacity to scale, customize, and deliver in accordance with stringent global trade compliances and audit frameworks.
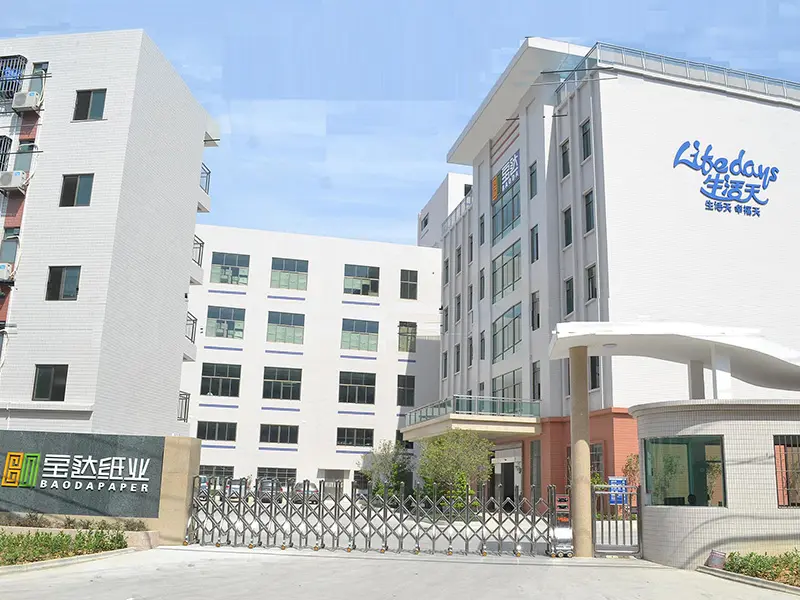
Uncovering the economic drivers, materials science innovation, and supply chain strategies determining success in the global sanitary tissue market.
Global demand is split between premium 100% virgin wood pulp and eco-conscious recycled or bamboo fibers. We utilize high-yield refining methods to construct soft, high-tensile base sheets that perform consistently under tensile stresses while optimizing raw material footprints.
With our robust infrastructure based in China, we leverage integrated port logistics and long-term pulp vendor alliances to insulate client brands from market disruptions, ensuring consistent pricing and prompt delivery even during times of macro supply chain strain.
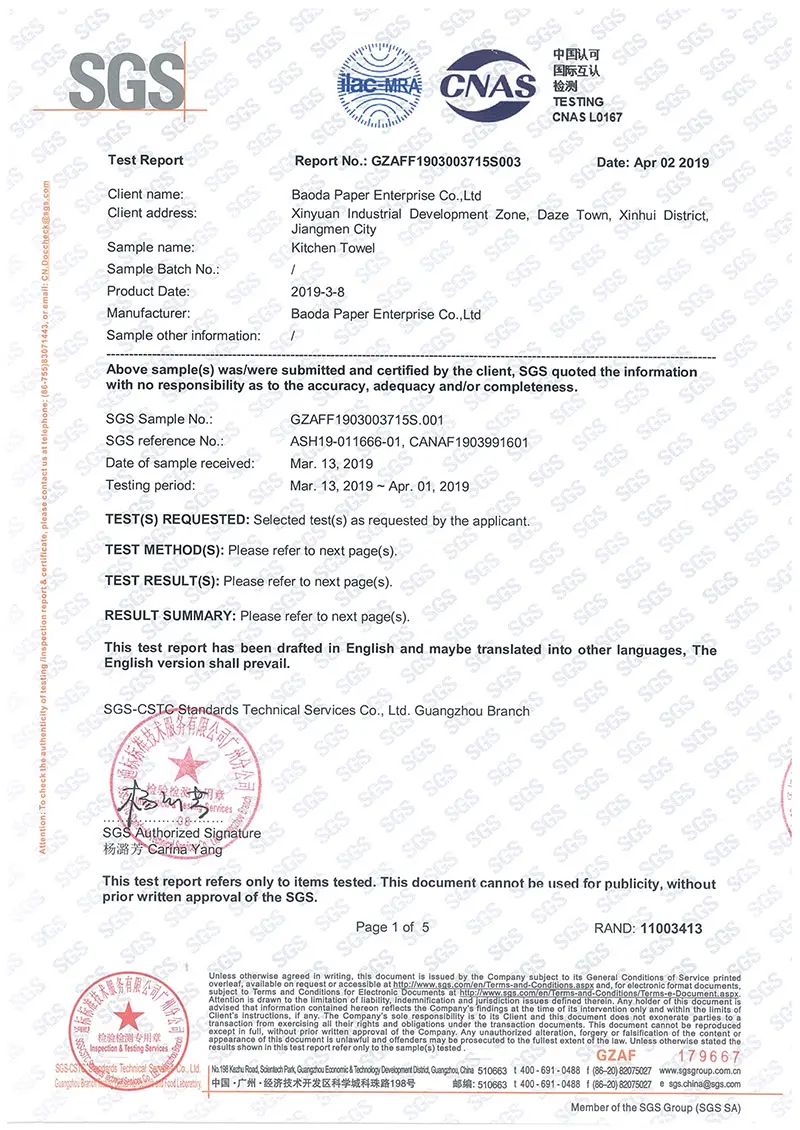
Certified in compliance with global standards, Baoda maintains a stringent multi-tier quality control protocol. From raw fiber testing to sheet formation, embossing roll precision calibration, and final packaging checks, zero defects is the goal.
Understanding the micro-structure of premium tissue reveals our commitment to advanced engineering. Our plant implements precise Yankee Dryer cylinder speed controls and creping blade angles to customize bulk, elasticity, and hand-feel. When laminating multiple plies, we utilize advanced water-soluble glue lamination networks to yield high water absorbency and structural stability without using harsh chemical additives.
Our future roadmap emphasizes integrated automation (Industry 4.0). We are gradually transitioning our packaging lines to smart robotics to reduce manual contact, ensuring clean, hygienic conditions. Furthermore, our R&D team is testing biodegradable plastic alternatives for outer wraps, answering the global demand for circular economy packaging.
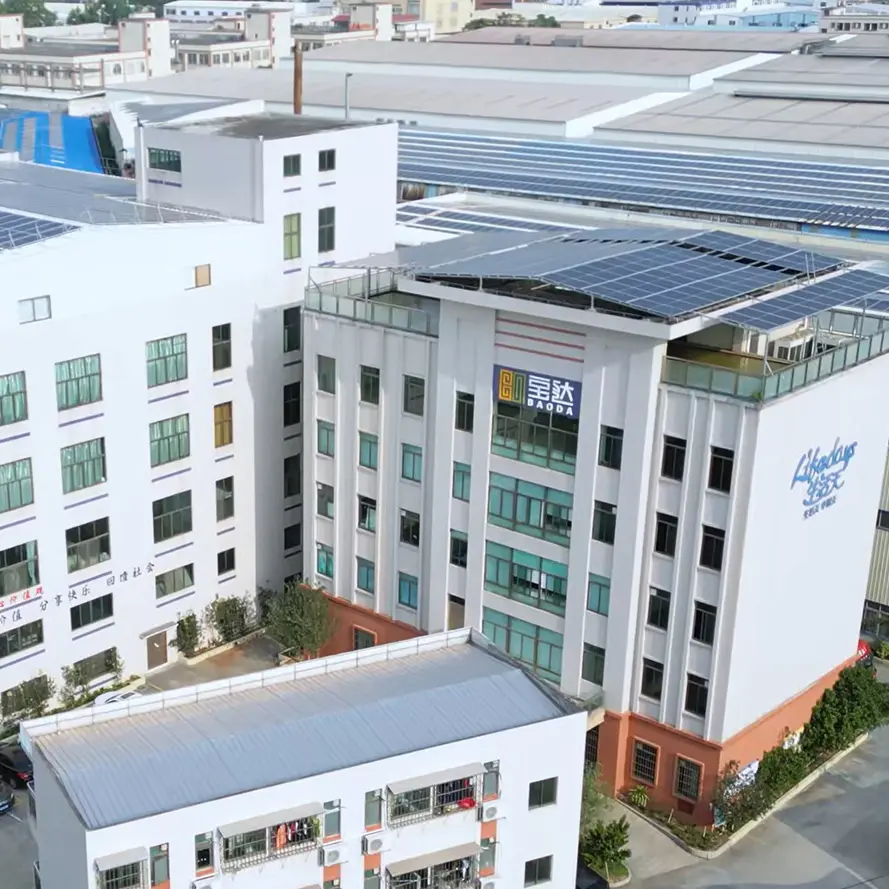
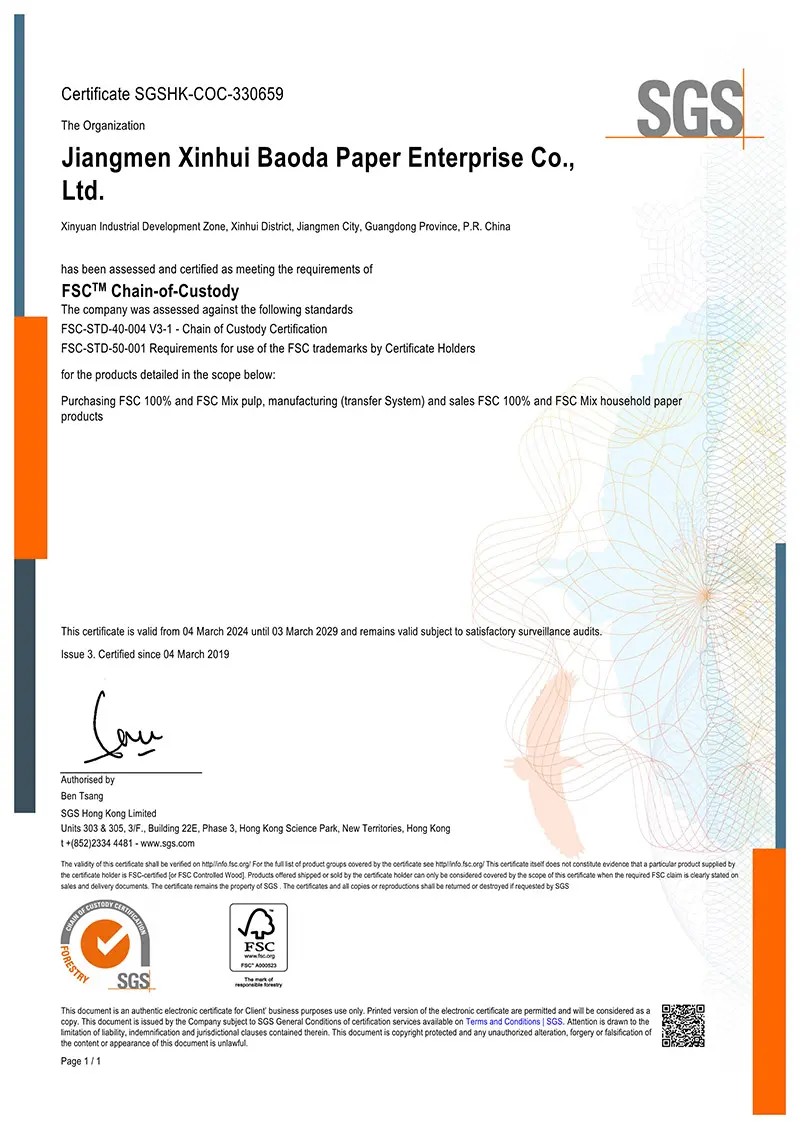
Our operation prioritizes environmental sustainability. We minimize our carbon footprint by utilizing water closed-loop recycling systems, significantly cutting water intake per ton of finished paper. Working directly with FSC (Forest Stewardship Council) certified suppliers, we verify that our pulp supplies are sourced from responsibly managed forests.
This commitment is not only ethical; it constitutes a crucial component of modern corporate value chains. Major brands like Walmart and Watsons rely on our certified processes to meet their own sustainability targets, providing transparent audit trails from raw materials to store shelves.
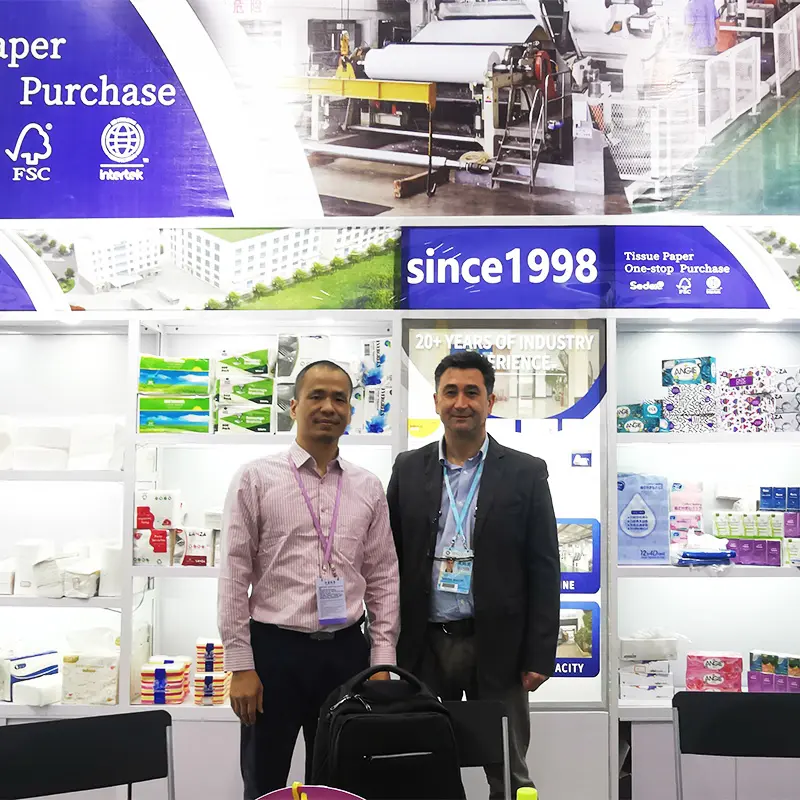
Different markets present distinct regulatory, physiological, and commercial expectations. We adapt our configurations to optimize local performance.
Our solutions for hotels and offices emphasize cost control, ease of dispensing, and compatibility with standard wall-mounted fixtures. Features include precise sheet perforations and high-yield core constructions.
For supermarket chains, shelf visual appeal is critical. We deliver customized embossed designs, multi-ply thick options (3-ply or 4-ply), and custom retail packaging formats that stand out on retail shelves.
We supply pure virgin pulp tissues that are free from optical brighteners, artificial fragrances, or chlorine bleaching residue, making them safe for sensitive skin types and medical facilities.
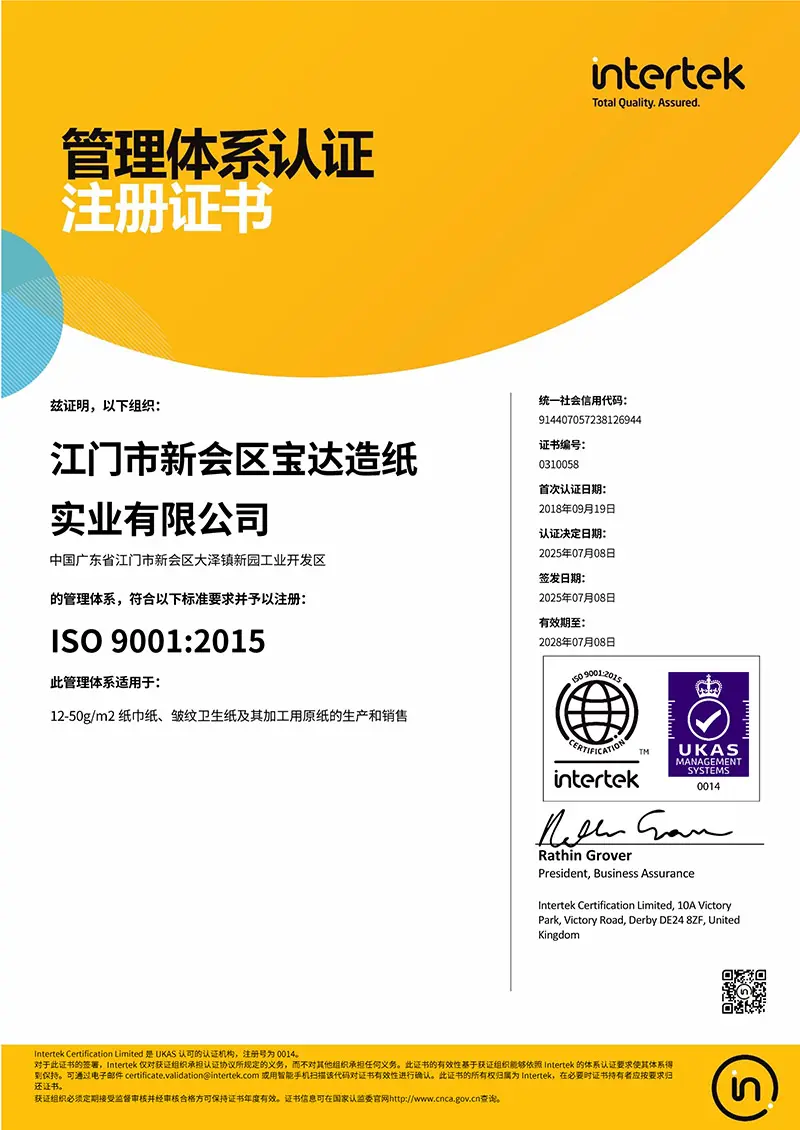
Our commitment to internationally recognized manufacturing practices is confirmed by leading verification credentials.
Key information regarding MOQ, factory capabilities, custom packaging, and supply chain logistics for B2B buyers.
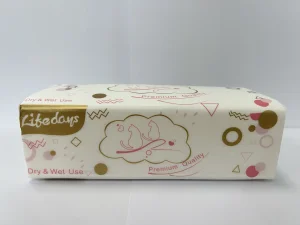
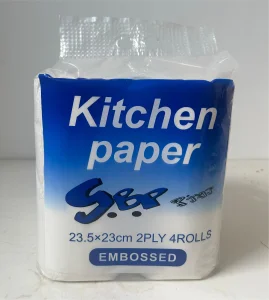
Explore our facial tissues, kitchen towels, napkins, and industrial solutions designed to fulfill everyday hygienic needs.
 BAODA PAPER