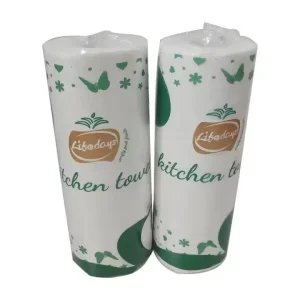
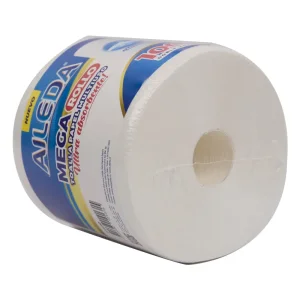
Explore our top-tier paper solutions built on international manufacturing excellence and optimized for global enterprise supply chains.
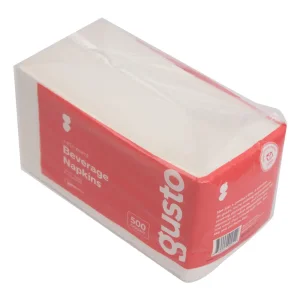
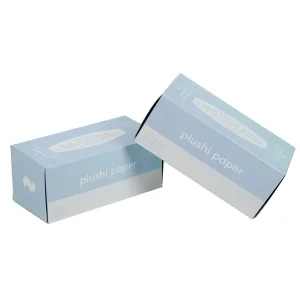
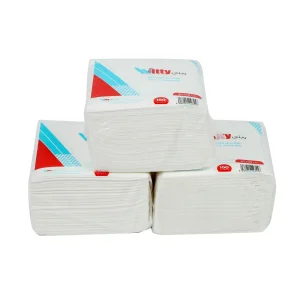
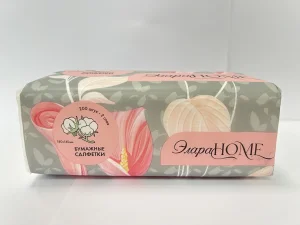
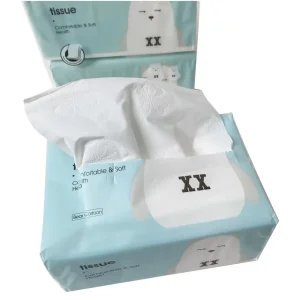
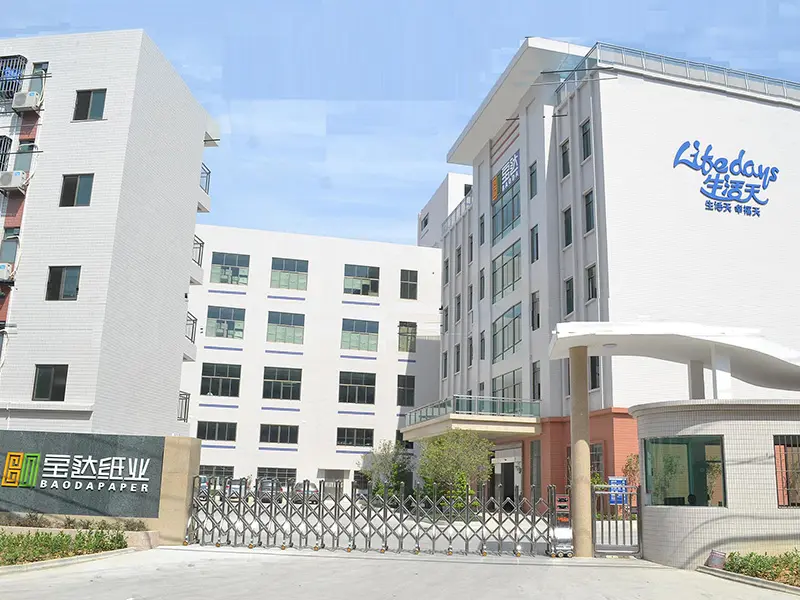
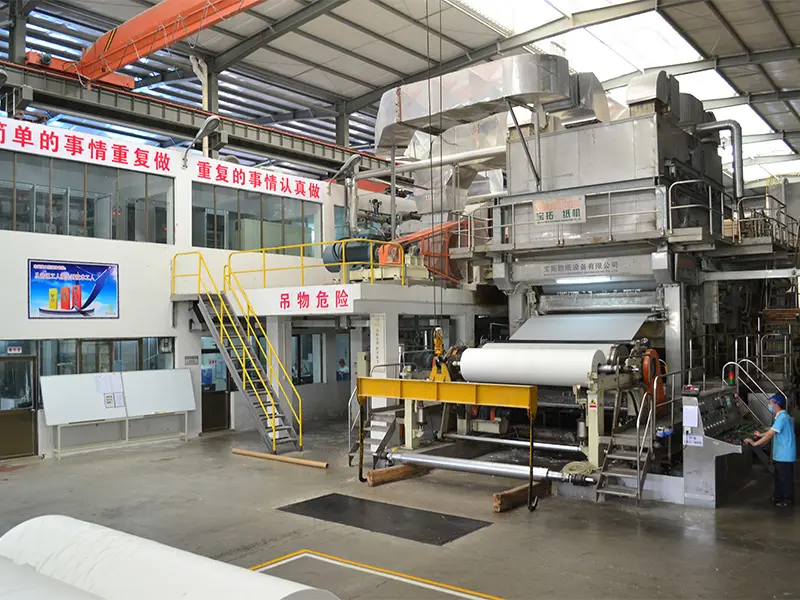
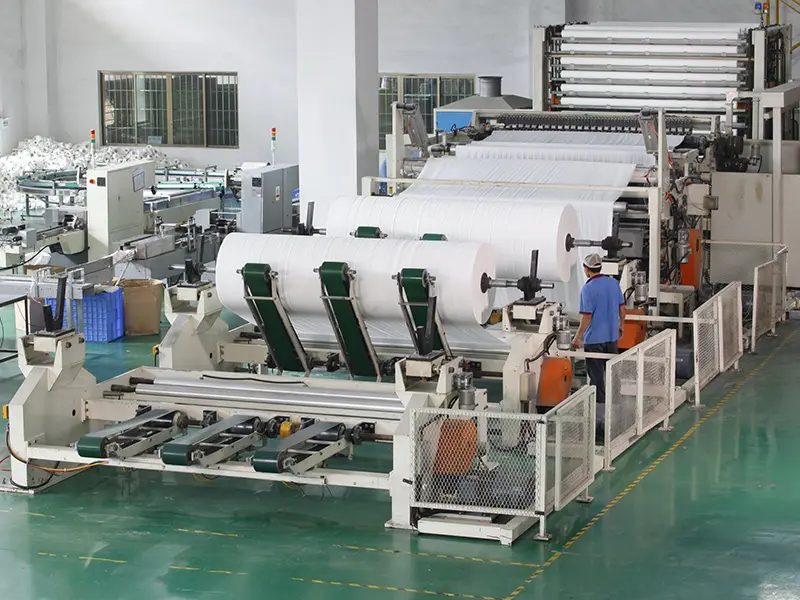
For over 27 remarkable years, since our inception in 1998, Baoda Paper Co., Ltd. has stood as an unwavering cornerstone of China's tissue paper industry, evolving from a domestic manufacturer into a globally recognized force. We have meticulously built our legacy on a formidable foundation of advanced manufacturing excellence and an unwavering commitment to quality. Our modern, sprawling complex, exceeding 20,000 square meters, is a testament to this commitment. Within its walls, we house state-of-the-art, imported high-speed paper machines and sophisticated automated processing lines. This powerful infrastructure is the engine behind our impressive annual production capacity of over 30,000 tons, enabling us to meet large-scale demands without compromising on the consistent quality that defines the Baoda name.
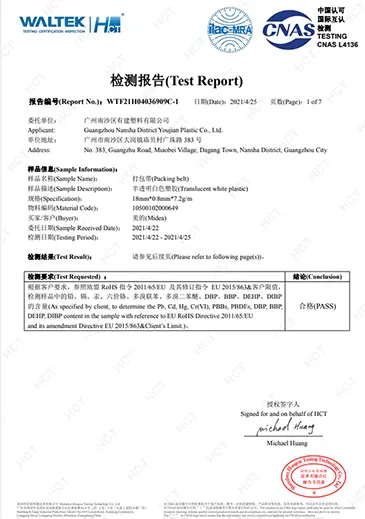
We process 100% virgin wood fiber to maximize the tensile strength and softness metrics, certified by regional testing agencies to ensure consistency across batches.
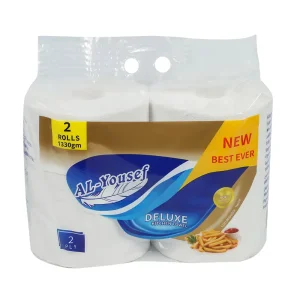
Our comprehensive and curated product portfolio is designed to provide complete one-stop solutions for diverse market needs. We offer an extensive range of products, from essential household items like premium toilet rolls, versatile kitchen towels, and soft facial tissues to convenient and hygienic pocket tissue packs for on-the-go use. Understanding the diverse paths to market success, our business model is both robust and flexible. While we proudly market three successful self-owned brands, we are also a premier partner for clients seeking to build their own product lines. We specialize in tailored ODM (Original Design Manufacturing), OEM (Original Equipment Manufacturing), and OBM (Original Brand Manufacturing) services, working collaboratively to bring our clients' unique visions and brand identities to life with precision and expertise.
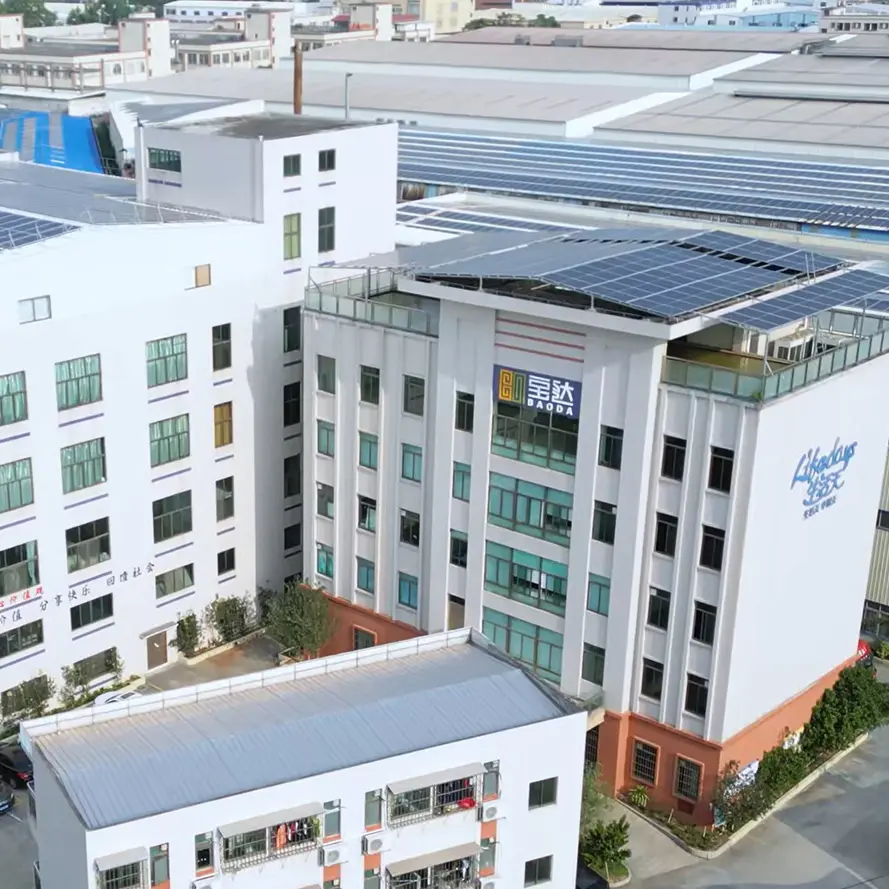
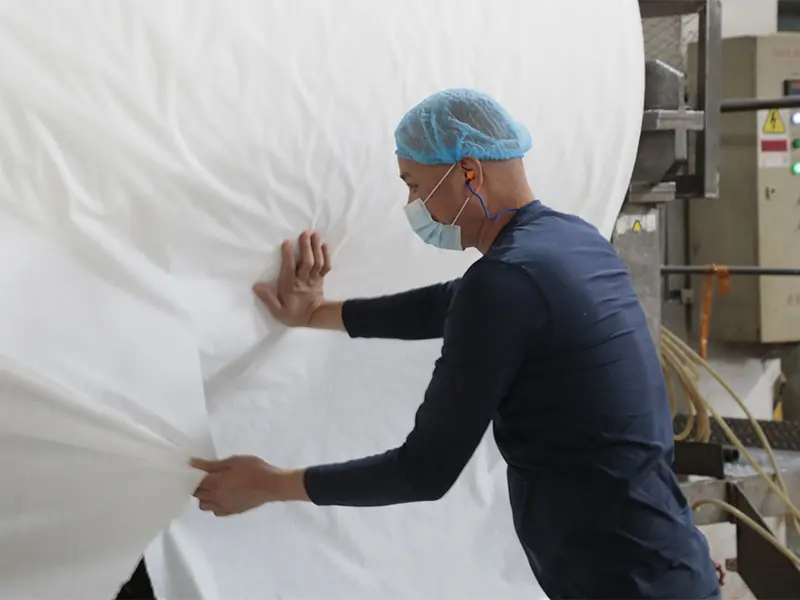
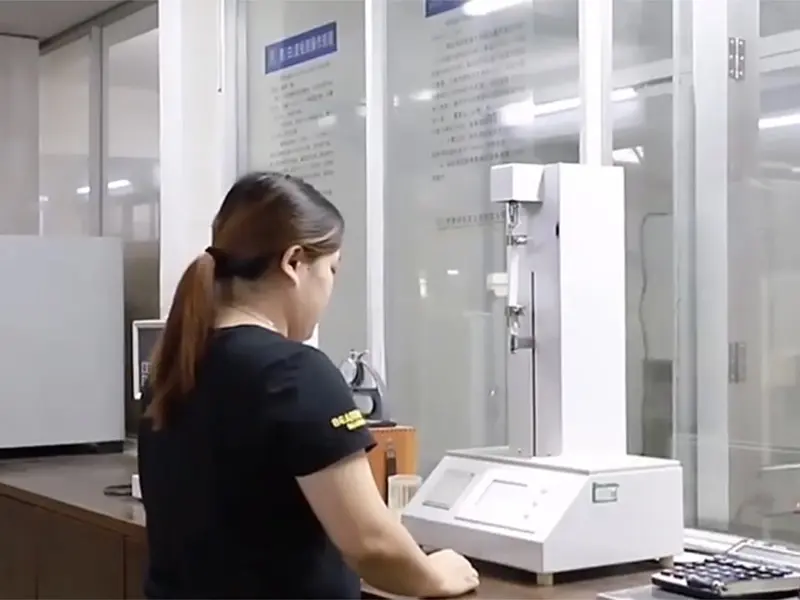
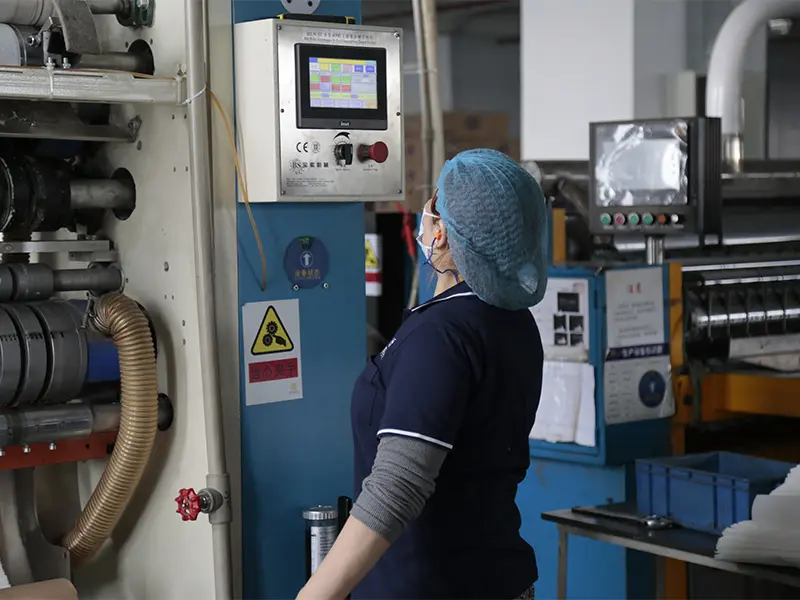
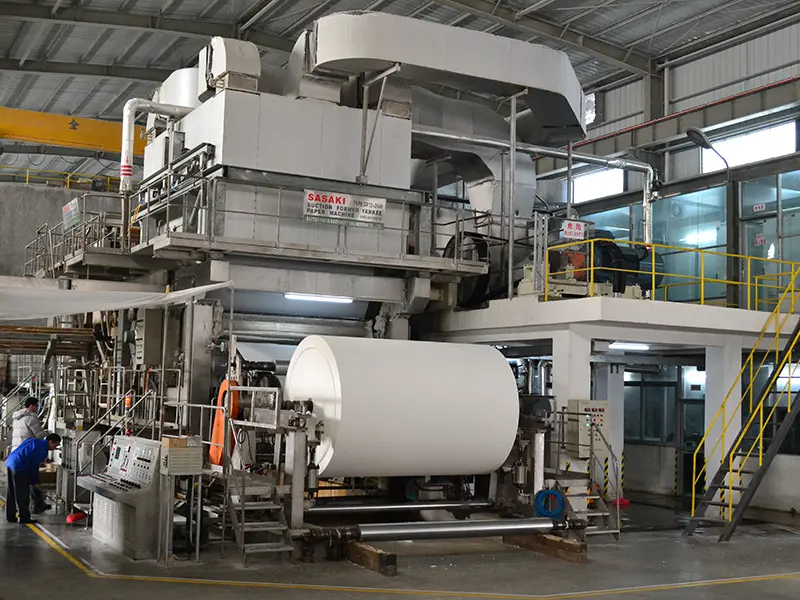
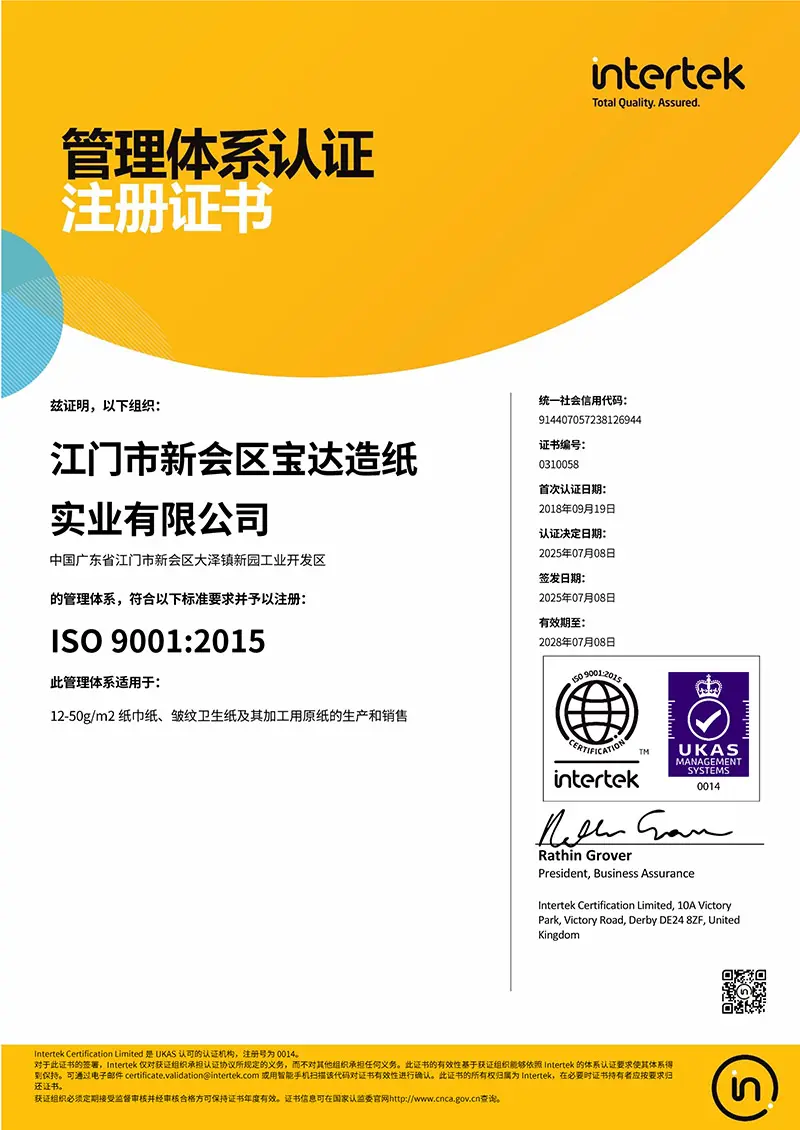
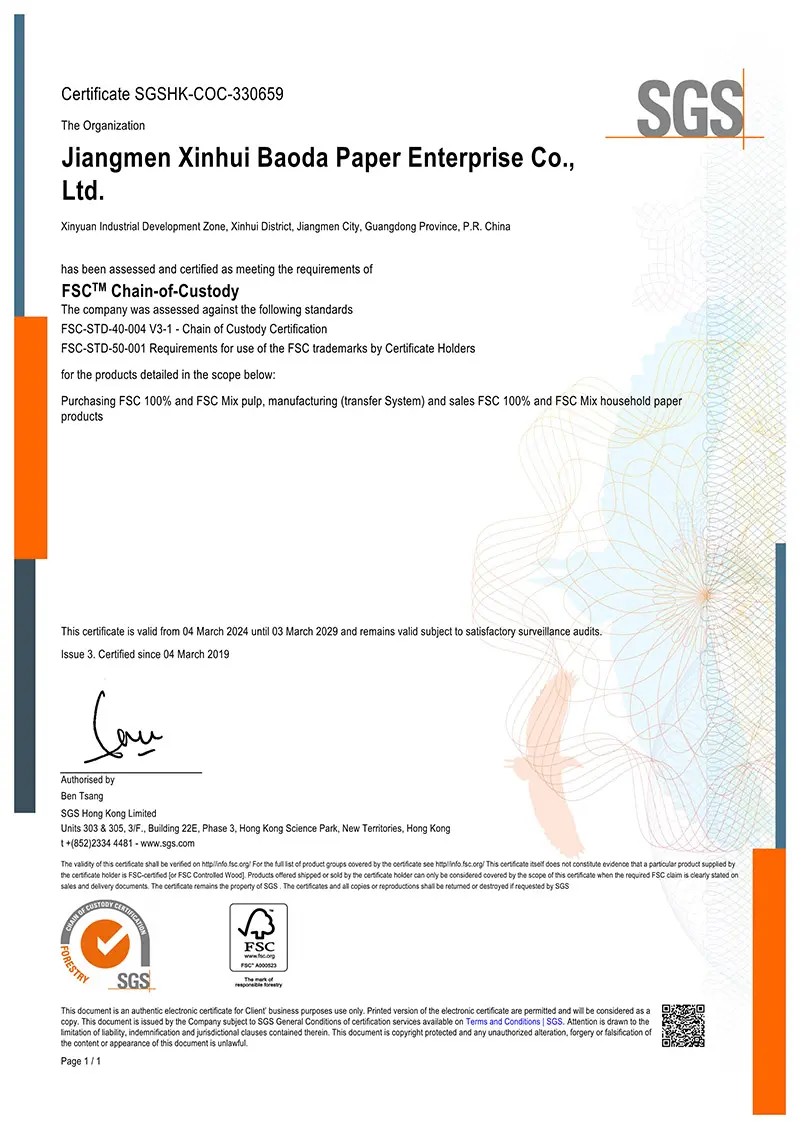
We align our industrial footprint with world-class standardizations and stringent social responsibility goals.
This dedication has earned us the trust of a vast network of over 10,000 global leaders in retail and distribution, including renowned giants such as Walmart and Watsons. We enforce circular water management to limit ecological impact.
Our high-quality products and reliable service have enabled us to build a robust international distribution network spanning more than 60 countries across the Americas, Europe, Asia, and Australia, with significant presence in key markets like the United States and Australia.
Through decades of innovation and consistent delivery, Baoda Paper has become more than just a manufacturer; we are a symbol of quality, reliability, and partnership in the dynamic global tissue market. Every consignment undergoes pre-loading stress assessments.
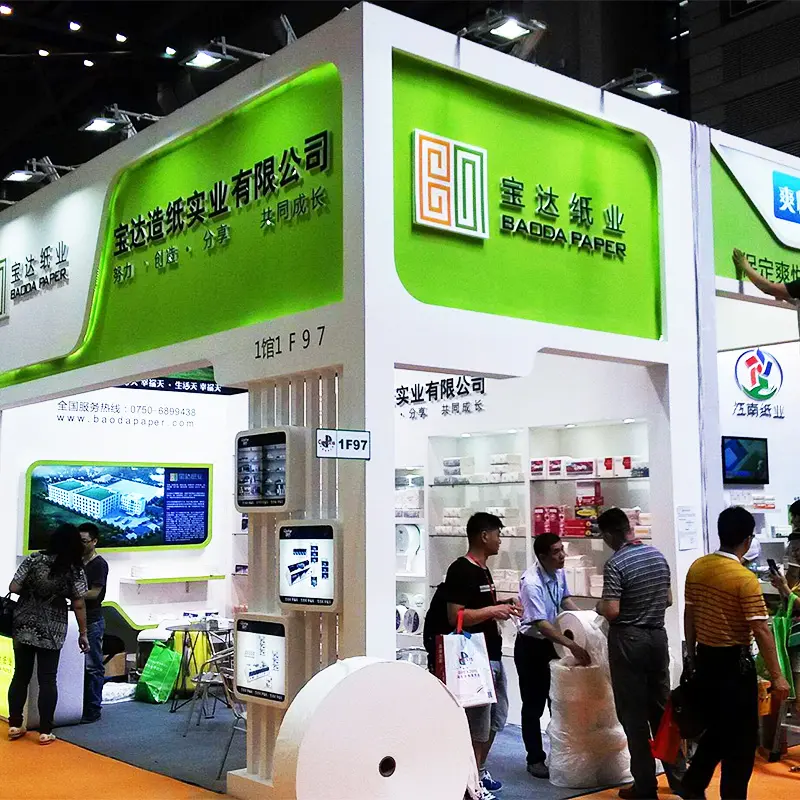
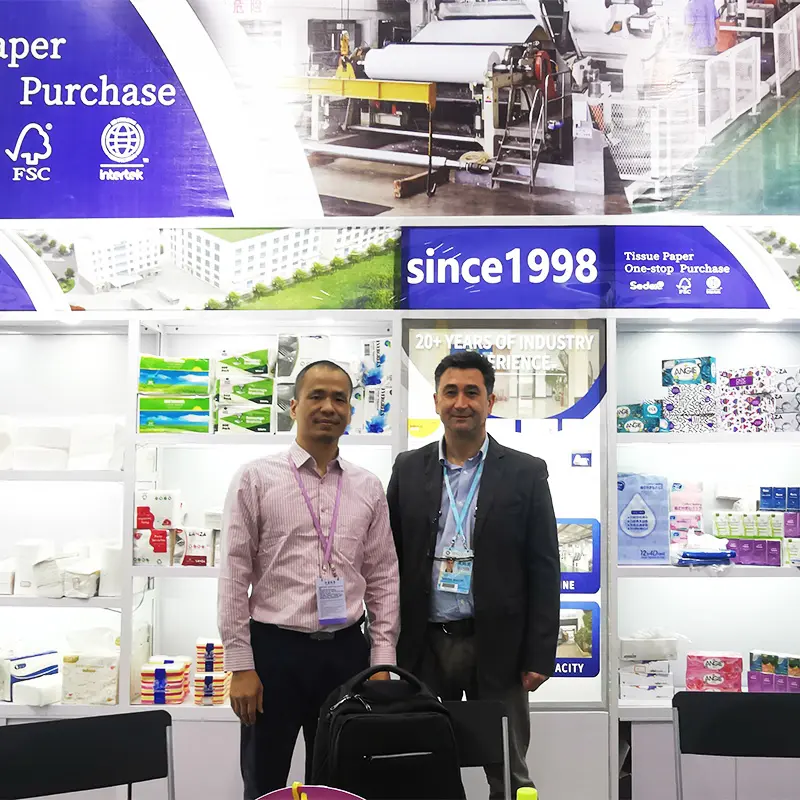
Why leading retail conglomerates and hospitality giants base their core volume supply chains in modern Chinese industrial clusters.
From global wood pulp procurement and chemical additive refinement to advanced logistics networks, our location in China's prime manufacturing zone ensures minimal lead times. The presence of container terminals minimizes overland shipping costs, allowing us to offer highly competitive pricing structures for multi-ton, high-volume orders.
Our production lines integrate micro-embossing technology with electronic tension control. This automated process minimizes variations in paper density, roll diameter, and perforation quality. High-capacity machinery allows us to complete large-scale OEM orders in fractions of the time taken by regional suppliers.
We offer extensive customization, including sheet dimensions, roll density, ply configuration (ranging from 1-ply up to 4-ply structures), and customized embossing patterns. This flexibility allows us to serve varied client requirements, from high-tensile kitchen rolls to soft facial tissues and premium quilted toilet papers.
An analysis of technological developments, sustainability demands, and procurement updates in the global sanitary paper industry.
Traditional flat paper rolls are increasingly being replaced by high-bulk quilted alternatives. Micro-embossing techniques lock multiple plies together using mechanical bonding or food-grade starches, rather than heavy chemical adhesives. This creates air pockets that increase absorbency by up to 30%, allowing buyers to reduce overall paper consumption while improving user comfort.
Global retailers are demanding fully traceble supply chains. Compliance with the Forest Stewardship Council (FSC) is now standard, and we are seeing a shift toward plastic-free paper packaging. Many markets are requiring biodegradable wraps or recycled content films to align with regional environmental legislation.
For high-traffic commercial dispensers, roll collapse can lead to jammed mechanisms and increased waste. Modern manufacturers are optimizing core stiffness and winding tension using computerized monitoring. This ensures rolls retain their cylindrical shape during marine shipping and high-humidity warehouse storage, protecting your investment.
To ensure high flushability alongside high wet absorbency, we balance long-fiber conifer pulp with short-fiber broadleaf pulp, ensuring the product breaks down efficiently after disposal.
We tailor our production parameters to match the unique cost-in-use and performance metrics of different target markets.
High-occupancy office towers require high-capacity, low-maintenance configurations. We supply tightly wound rolls with high sheet counts to minimize restocking frequency. Core diameters are engineered to fit standard commercial multi-roll dispensers, and clean perforations help reduce excess usage.
Premium hotels require soft, high-bulk paper. We supply 3-ply and 4-ply quilted options made from 100% virgin pulp, featuring custom micro-patterns and decorative border embossing. This provides a soft texture and high absorbency, supporting a premium guest experience.
For large retail brands, shelf presence and consistent packaging are key. We support private-label lines with customized retail packaging, barcode integration, multi-pack configurations (e.g., 4-pack, 12-pack, 24-pack), and promotional print wraps, all conforming to local regulatory standards.
For B2B buyers, category managers, and supply chain directors, sourcing sanitary paper requires rigorous verification of technical and compliance metrics. Use our operational checklist to review your prospective manufacturer:
Our QA process begins at the pulp mill and continues through to final shipment. We run on-line optical inspections to identify and remove any sheets with pinholes or dust particles. Automated sensors continuously monitor embossing depth and ply adhesion to ensure consistent physical properties across every batch we produce.
Our facilities maintain ISO 9001, ISO 14001, and social compliance certifications, simplifying the audit process for international buyers.
Get answers to technical questions about fiber sourcing, customization, bulk lead times, and logistics.
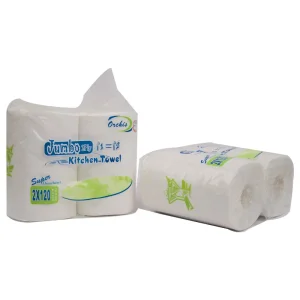
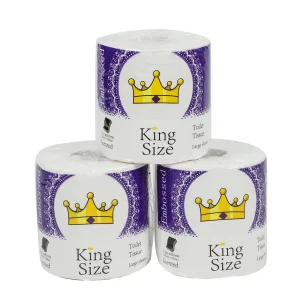
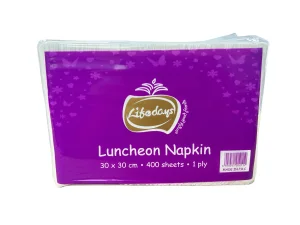
High-absorbency, high-tensile kitchen rolls, napkins, and tissues designed for intensive B2B commercial applications.
 BAODA PAPER