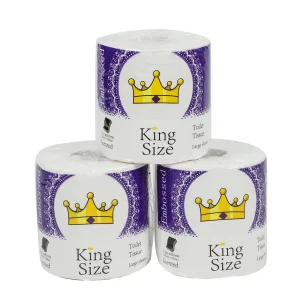
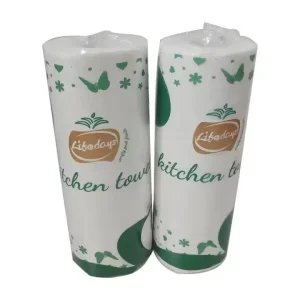
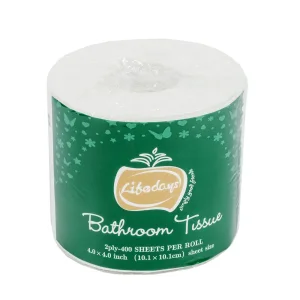
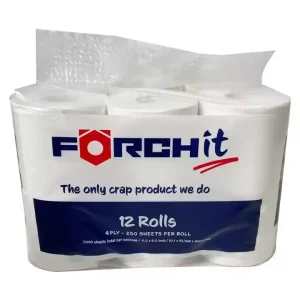
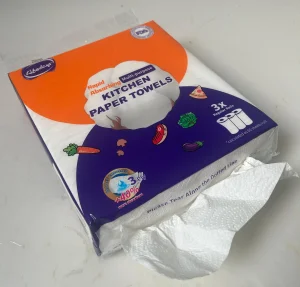
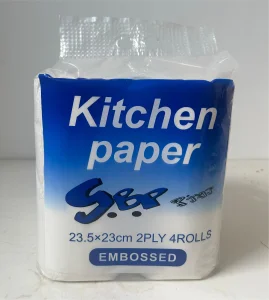
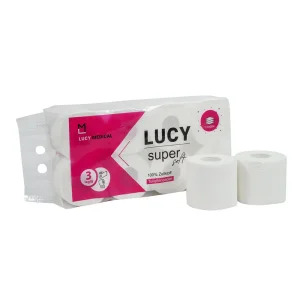
Engineered for absolute strength, softness, and instant dispersibility in diverse commercial and home applications.
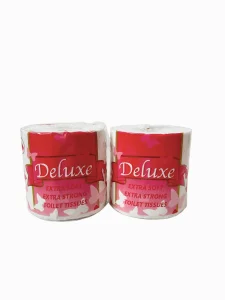
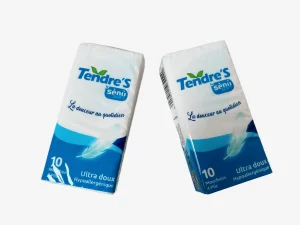
How advanced raw materials and high-efficiency manufacturing technologies are shaping the future of global B2B tissue exports.
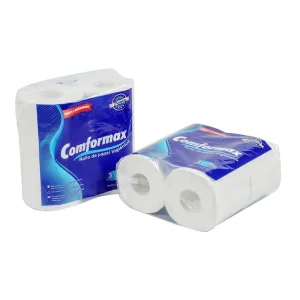
The commercial and domestic hygiene paper sector is undergoing a massive transformation driven by changing consumer behaviors, stricter environmental policies, and dynamic supply chain economics. "Small Toilet Paper" products, once treated as minor commodities, have transitioned to the center of product design. As retail giants and institutional buyers shift focus to waste minimization, material efficiency, and FSC-certified sourcing, tissue manufacturers must leverage cutting-edge material engineering. High-density, short-core, or coreless rolls are gaining rapid traction because they maximize structural density, optimize container storage space, and lower global freight emissions.
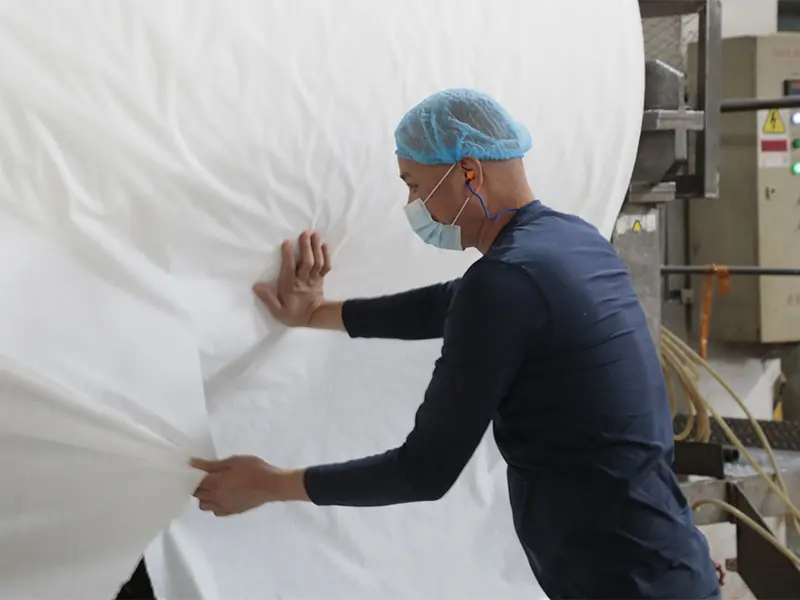
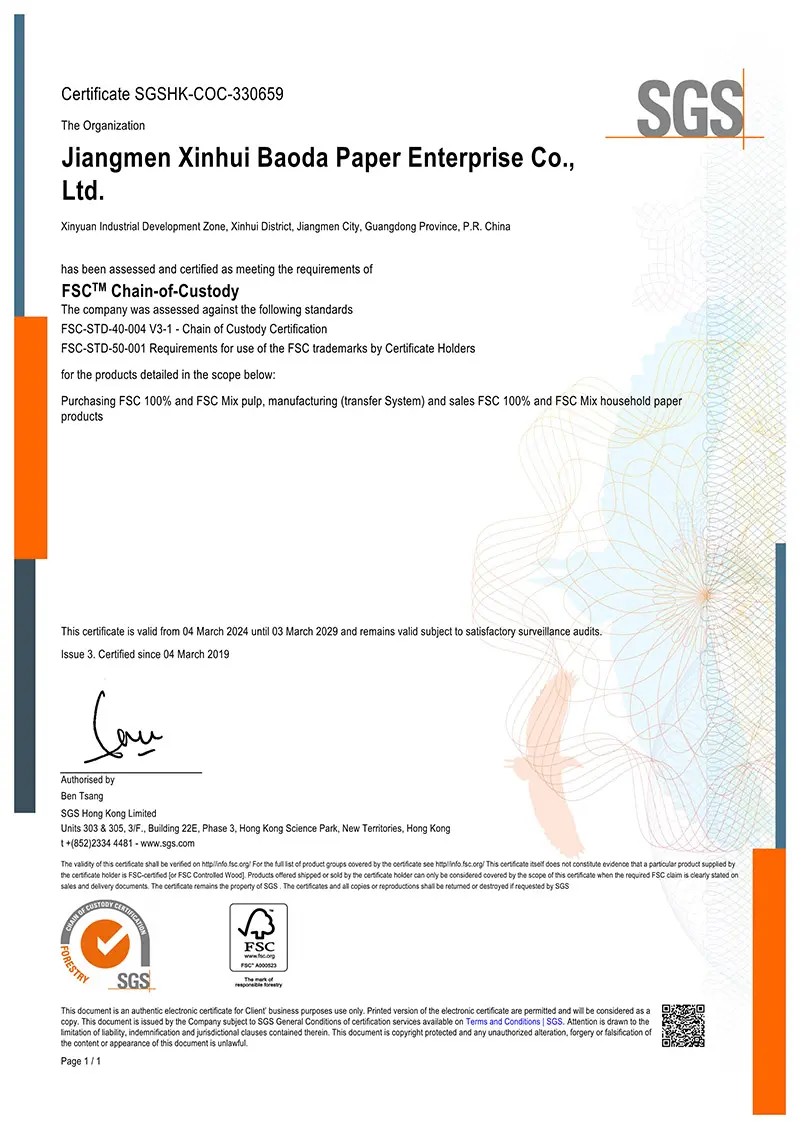
Consumers demand transparency in raw materials. Modern tissue manufacturing processes utilize 100% virgin pulp harvested exclusively from certified, responsibly managed forests to preserve biodiversity and prevent unauthorized deforestation.
By implementing micro-embossing techniques and multi-ply adhesive lamination, we increase mechanical thickness and moisture-absorption speed, delivering high strength while reducing total material usage.
Advanced high-pressure winding machinery compresses tissue rolls efficiently. This increases density, significantly reducing freight footprint and cutting overall storage costs for international distributors.
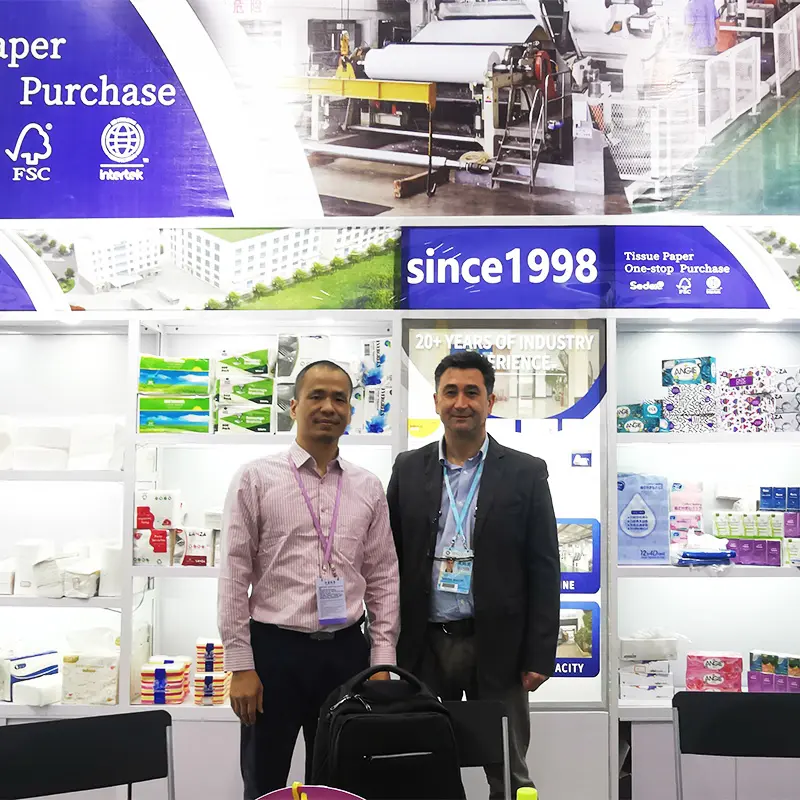
Established in 1998, Baoda Paper Co., Ltd. has developed into a premier force in the international paper industry. From our roots as a quality-focused regional manufacturer, we have evolved into a highly integrated export powerhouse. Over nearly three decades of continuous innovation, we have focused on manufacturing capability, strict quality management frameworks, and customer-first services.
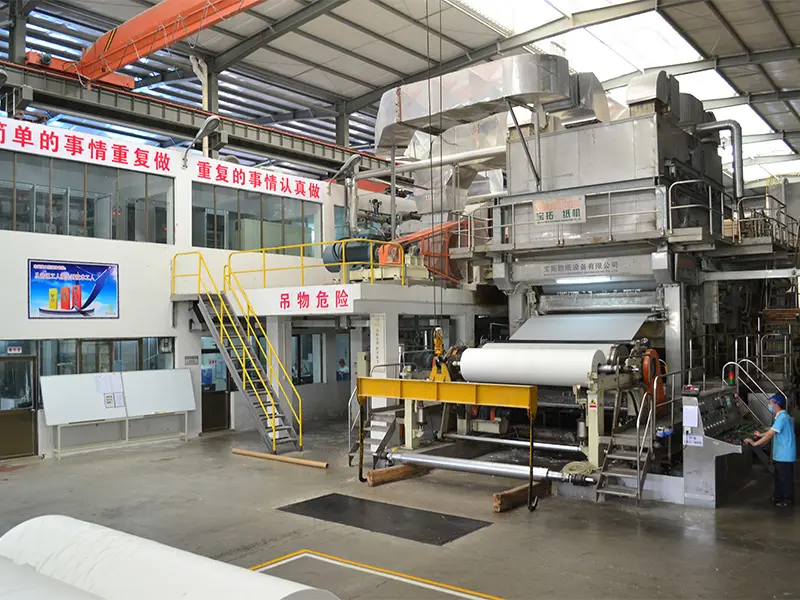
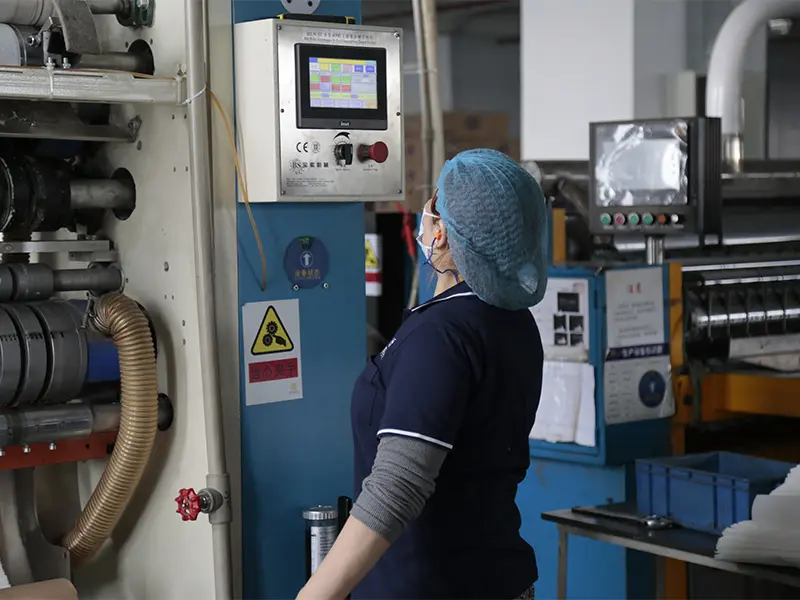
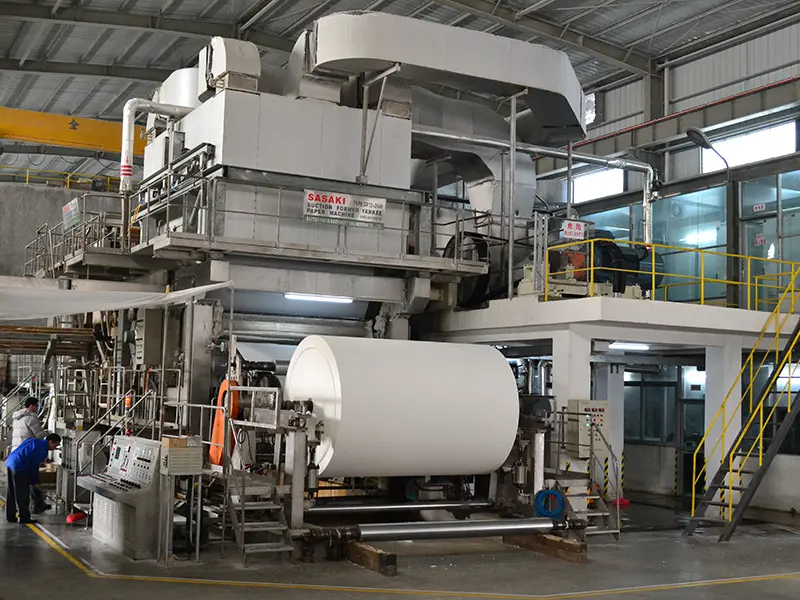
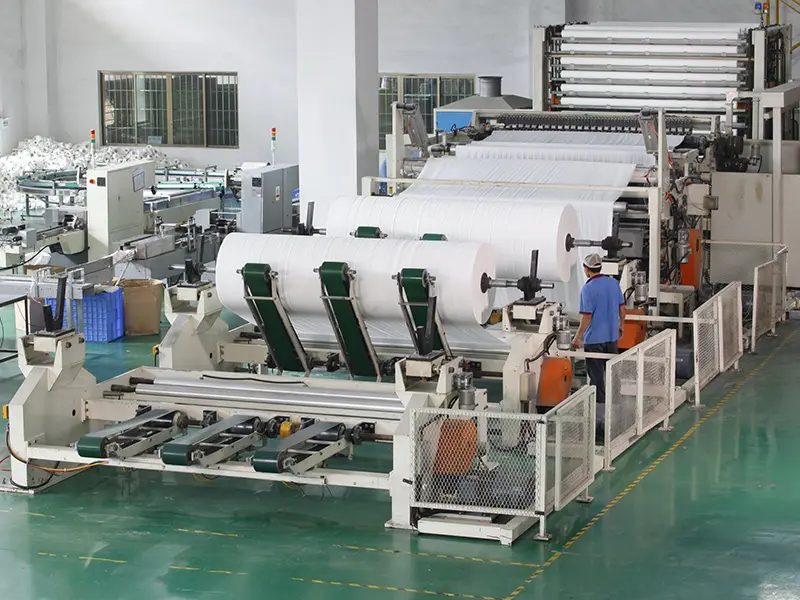
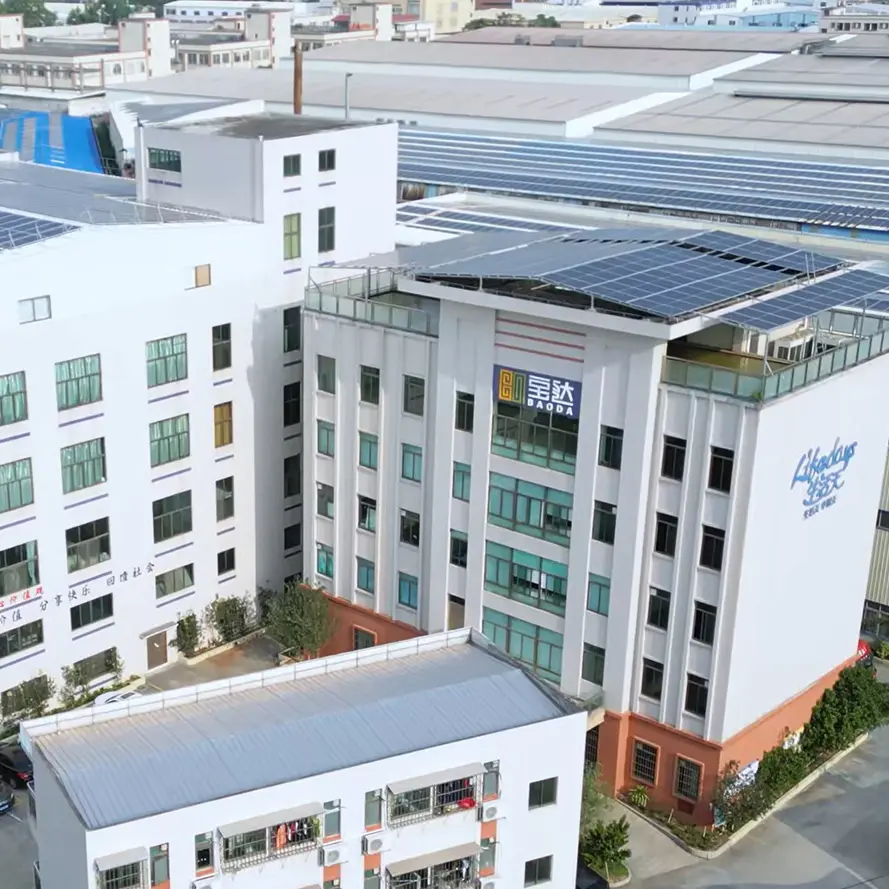
Our manufacturing site spans more than 20,000 square meters. It is equipped with imported high-speed Crescent Former paper machines, automated embossing setups, and advanced rewinding-packaging systems. This advanced setup produces an annual capacity of over 30,000 tons of high-grade paper, allowing us to process bulk orders without compromising on product quality.
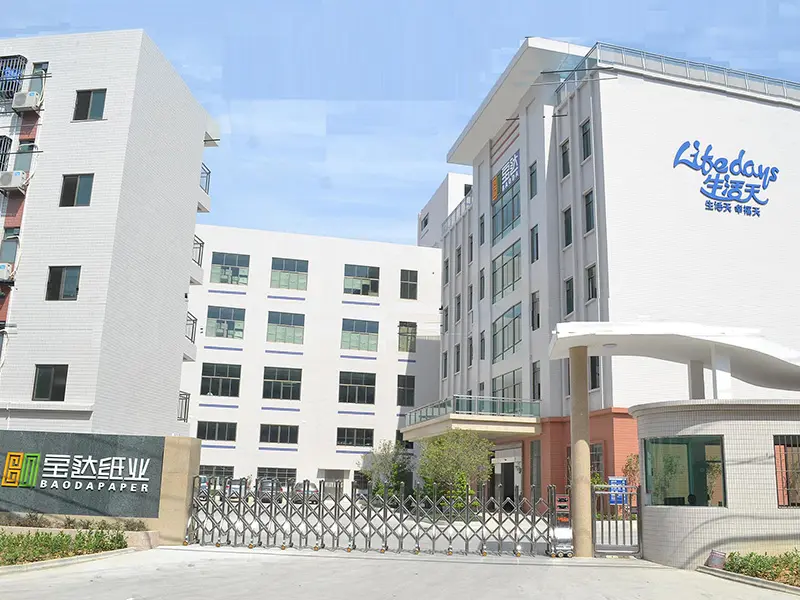
Understanding the diverse requirements of international markets, Baoda Paper operates on a flexible, highly customized business model. We offer complete OEM, ODM, and OBM services, helping global brands establish high-quality product lines.
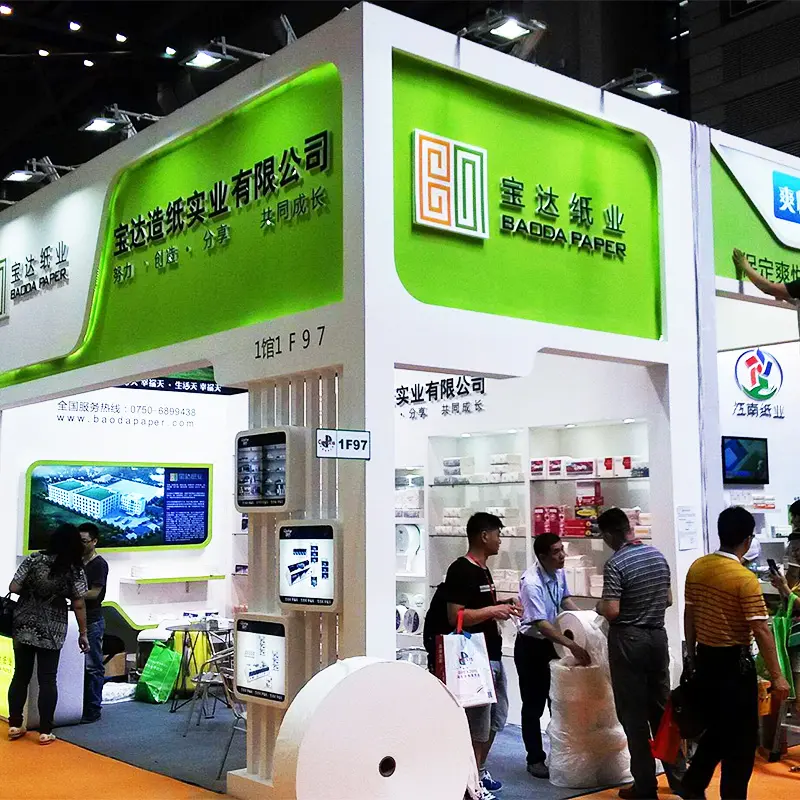
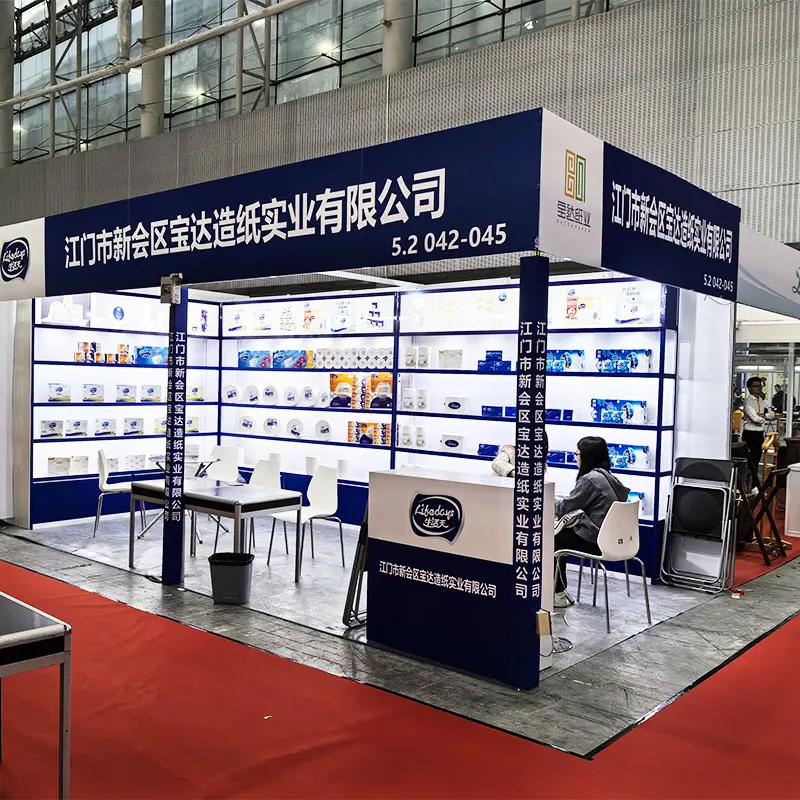
Our commitment to social responsibility and rigorous quality control has earned the trust of over 10,000 retail and distribution companies worldwide, including global chains like Walmart and Watsons. Today, our international sales network covers over 60 countries across the Americas, Europe, Asia-Pacific, and Australia, delivering consistent, reliable hygiene solutions.
Years of Manufacturing Experience
Annual Production Capacity (Tons)
Factory Floor Area (sqm)
Exporting Countries & Regions
Addressing complex supply chain challenges with reliable manufacturing processes and global logistical support.
Navigating international trade barriers, strict environmental regulations, and fluctuating freight logistics requires an experienced manufacturing partner. We offer end-to-end supply chain integration, from raw material procurement to custom customs clearances.
Through direct partnerships with international pulp suppliers, we secure long-term, high-quality material commitments. This keeps our production schedules stable and insulates our partners from market price fluctuations.
All virgin fibers are tracked through a robust custody chain to ensure compliance with green purchasing standards. This trace-and-track system supports corporate environmental initiatives for big-box retailers.
By engineering high-density roll structures and space-optimized outer cartons, we maximize shipping container volume. This helps clients reduce shipping costs and overall import fees.
How we plan to drive structural efficiency and green standards through 2030.
Integrating rooftop photovoltaic arrays and biomass heat recovery boilers to reduce manufacturing emissions by 35% across our paper mills.
Implementing advanced wastewater purification processes, recycling over 92% of production water to significantly reduce water consumption per ton of paper.
Expanding the production of high-density coreless rolls to minimize cardboard core waste and optimize international container space.
Establishing digital warehousing systems and real-time inventory management to accelerate transit times for overseas distribution partners.
Maintaining strict quality and environmental standards across our entire export operations.
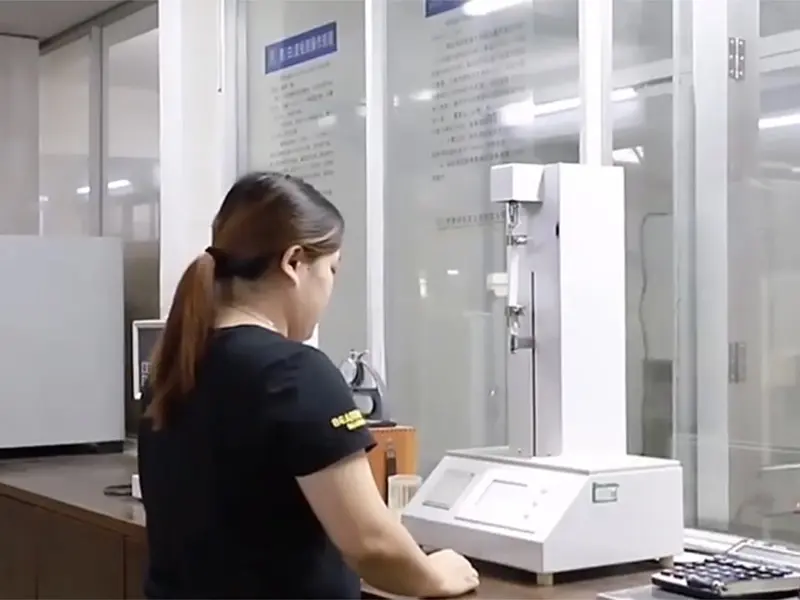
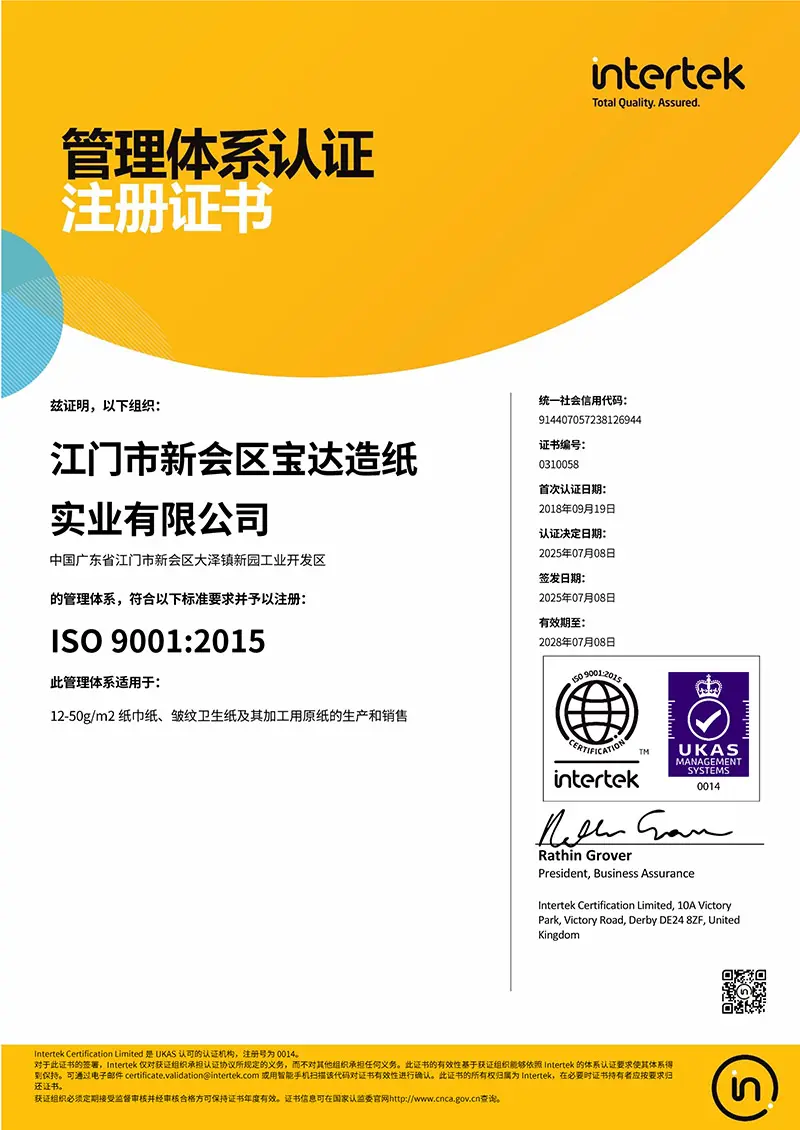
Our facility operates under rigorous international standards. We maintain formal quality systems to ensure our paper products comply with global trade requirements.
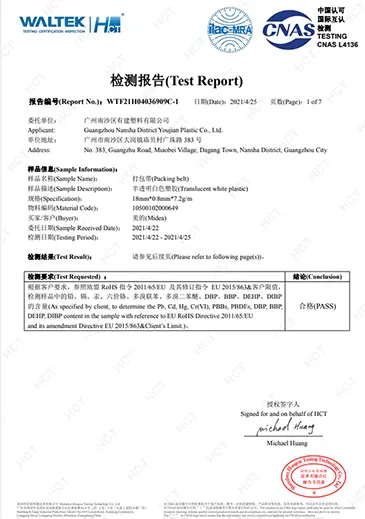 SGS System Certification
 Quality Standard Compliance
 ISO 9001 Certification
 ISO 14001 Certification
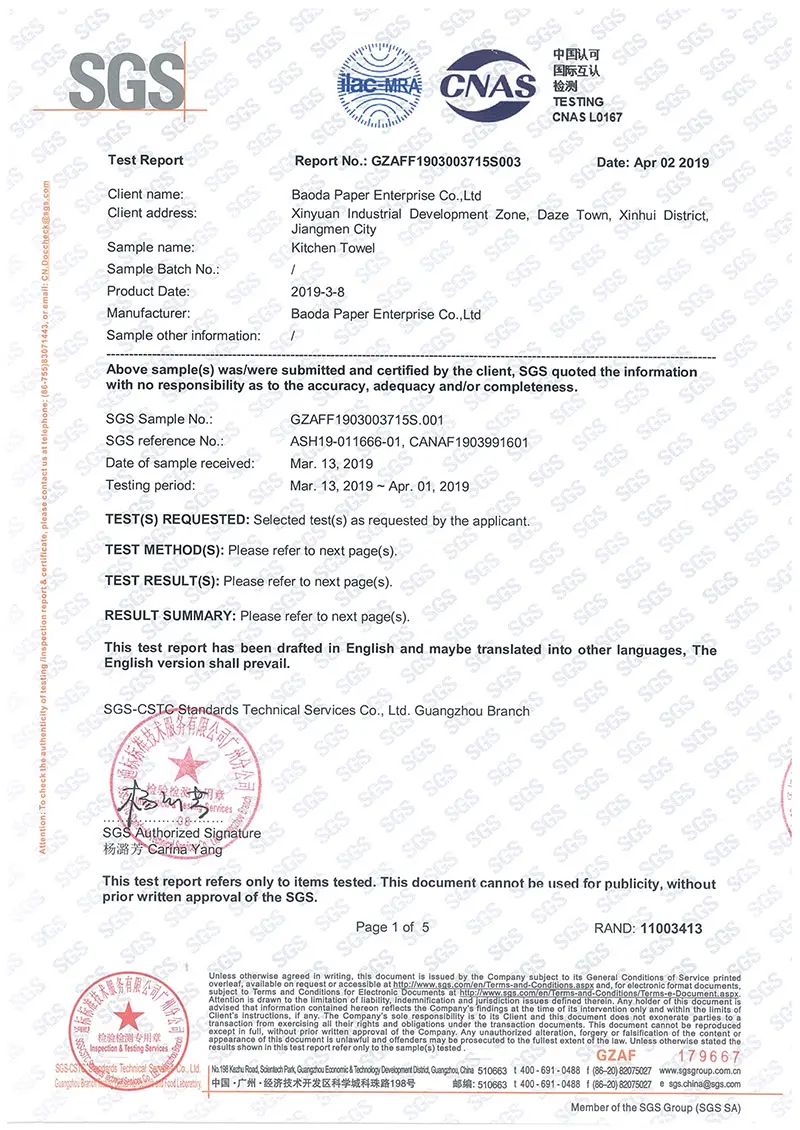 ISO 45001 Certification
Addressing top questions from global supply managers, procurement directors, and importers.
Exporters and factory direct pricing for specialized commercial rolls, kitchen towels, and napkins.
 BAODA PAPER