Engineered for maximum absorbency, tensile strength, and eco-friendly performance across industrial and domestic environments.
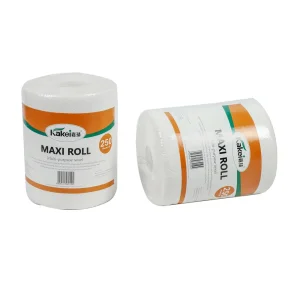
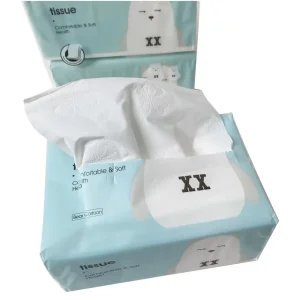
In the modern commercial tissue landscape, procuring high-performance paper towels transcends simple supply logistics. Today's commercial, hospitality, and residential markets demand products with exceptional tensile strength, fast fluid retention, and highly verified hygienic integrity. As premium paper towel suppliers, we focus on technical parameters such as basis weight (GSM), wet tensile strength indexes, and water retention capacity (WRC) to ensure our tissues perform consistently under demanding conditions.
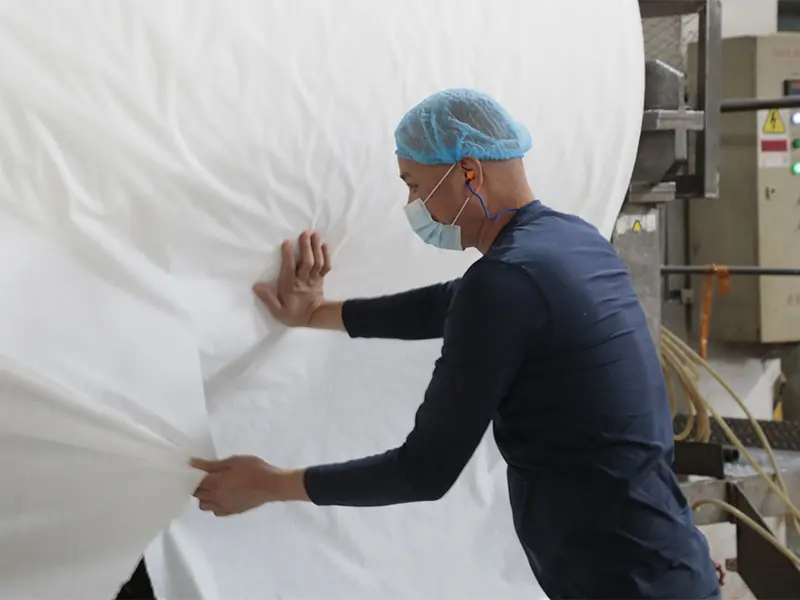
Our manufacturing protocols leverage advanced micro-embossing technology, introducing pocketed air barriers between plies. This increases the total volume capacity for liquid capture without increasing the raw pulp weight. For global distributors, this represents a crucial balance: offering lightweight, transport-efficient rolls that perform as well as heavier grades. This design optimizes container packing factors while lowering carbon footprints and overall shipping costs.
Dual-layer micro-embossing creates dynamic air pockets, enhancing liquid absorption by up to 250% compared to standard flat-sheet kitchen rolls.
Reinforced pulp blends ensure the tissue maintains structural integrity and resists tearing when fully saturated with oil, water, or commercial solvents.
Our raw fiber is sourced through certified, renewably managed forests, ensuring that every supply run aligns with strict environmental standards.
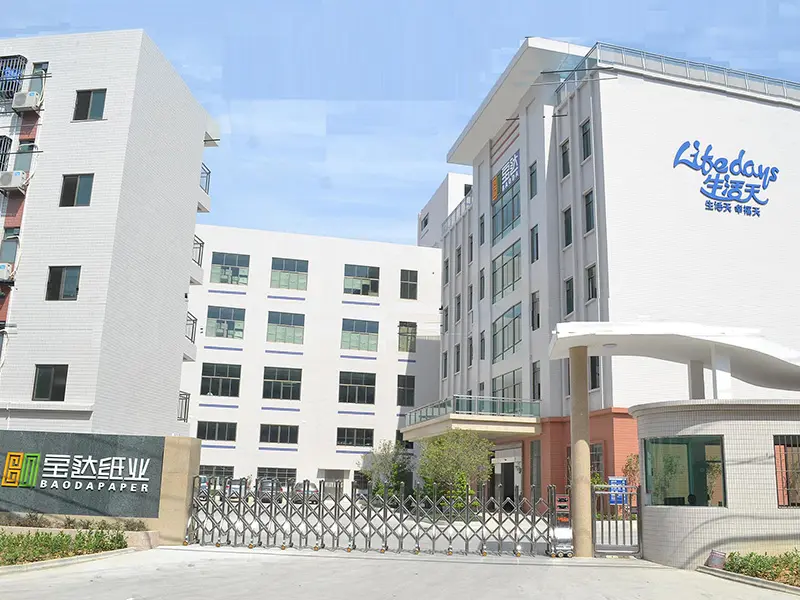
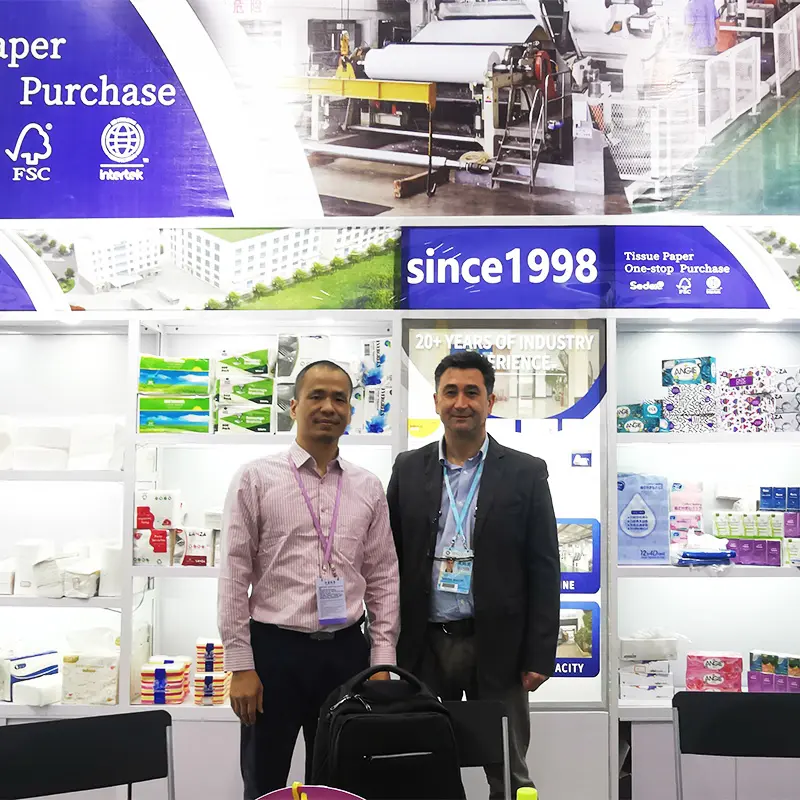
For over 27 remarkable years, since our inception in 1998, Baoda Paper Co., Ltd. has stood as an unwavering cornerstone of China's tissue paper industry, evolving from a domestic manufacturer into a globally recognized force. We have meticulously built our legacy on a formidable foundation of advanced manufacturing excellence and an unwavering commitment to quality.
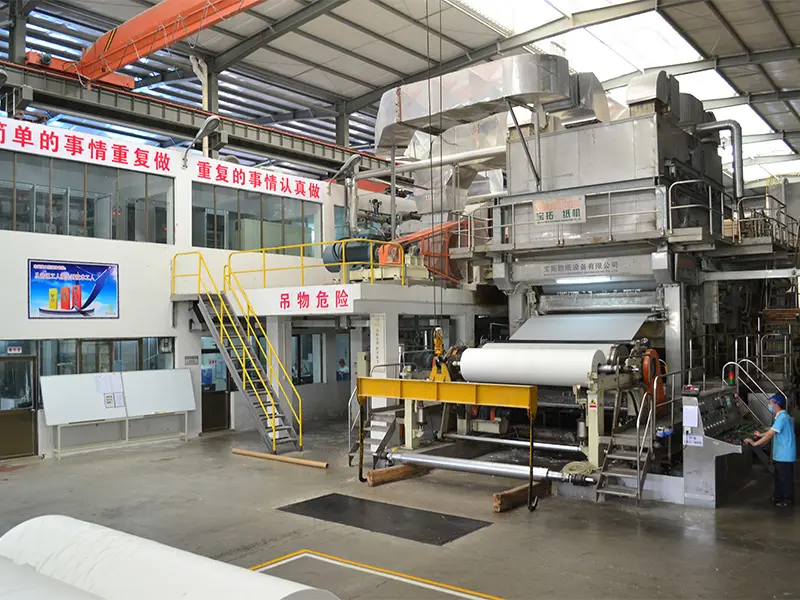
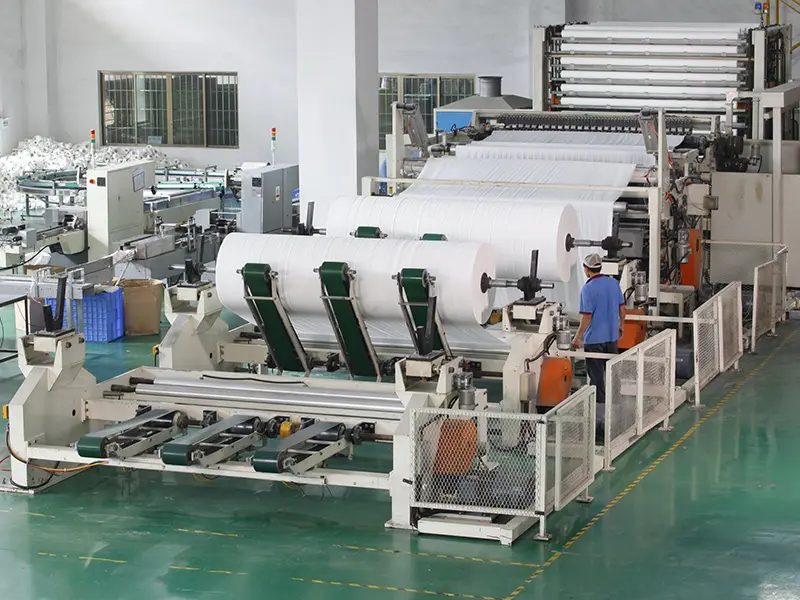
Our modern, sprawling complex, exceeding 20,000 square meters, houses state-of-the-art, imported high-speed paper machines and sophisticated automated processing lines. This powerful infrastructure is the engine behind our impressive annual production capacity of over 30,000 tons, enabling us to meet large-scale demands without compromising on consistent quality.
Our comprehensive and curated product portfolio is designed to provide complete one-stop solutions for diverse market needs. We offer an extensive range of products, from essential household items like premium toilet rolls, versatile kitchen towels, and soft facial tissues to convenient and hygienic pocket tissue packs for on-the-go use.
Understanding the diverse paths to market success, our business model is both robust and flexible. While we proudly market three successful self-owned brands, we are also a premier partner for clients seeking to build their own product lines. We specialize in tailored ODM (Original Design Manufacturing), OEM (Original Equipment Manufacturing), and OBM (Original Brand Manufacturing) services, working collaboratively to bring our clients' unique visions and brand identities to life with precision and expertise.
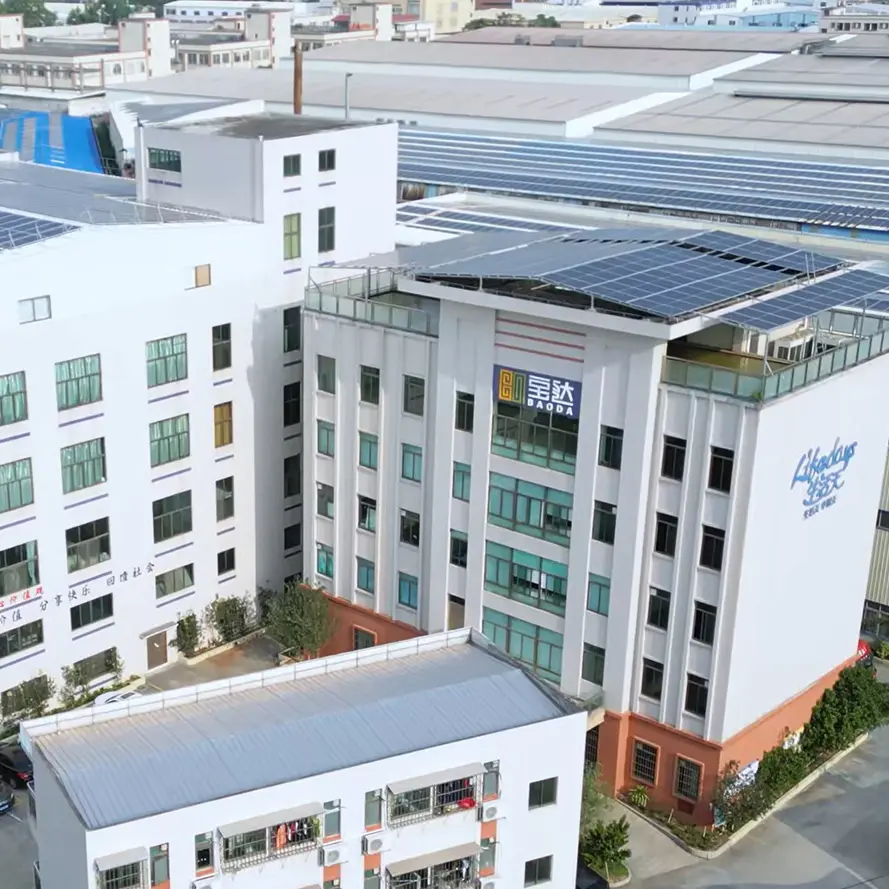
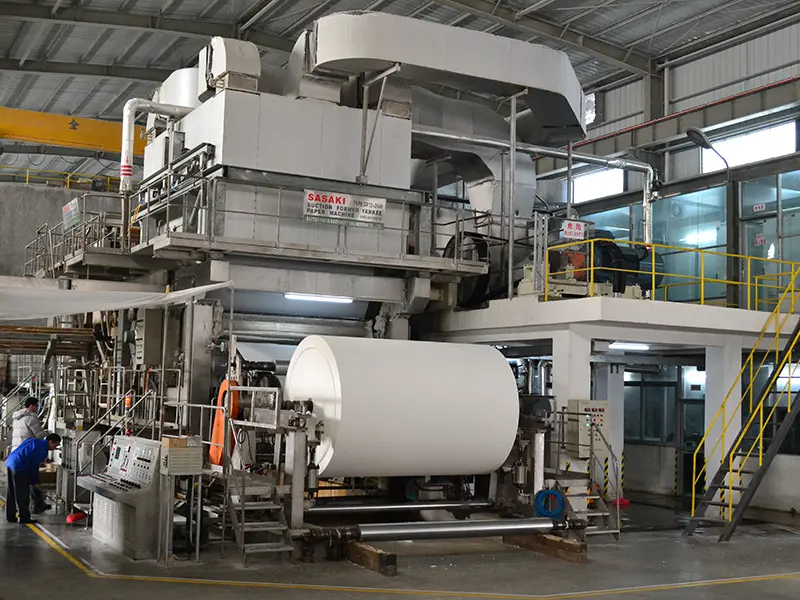
Decades of continuous refinement have allowed us to build an international supply chain network optimized for reliability and efficiency. Our core philosophy is built upon three pillars designed to support high-volume distributors:
Entering strict international markets requires compliance with comprehensive chemical, environmental, and food safety standards. We offer custom manufacturing services that adapt to the regulatory frameworks of the Americas, Europe, and Asia-Pacific.
Our kitchen paper towels meet strict food safety guidelines, including US FDA 21 CFR standards and European BfR XXXVI regulations, ensuring safe contact with food items.
We tailor sheets, roll dimensions, and sheet counts to match local preferences, supporting US standard rolls, EU slim rolls, and custom sheet configurations.
We offer certified wood pulp traceabilty, verifying that all input materials originate from forests audited for biodiversity preservation and ethical labor.
China's integrated tissue paper supply chain provides significant cost efficiencies, production agility, and scale. We combine regional supply network advantages with automated production processes to offer reliable, cost-effective solutions.
Close partnerships with international pulp mills secure our virgin softwood and hardwood pulp supplies, keeping raw material costs stable even during market shifts.
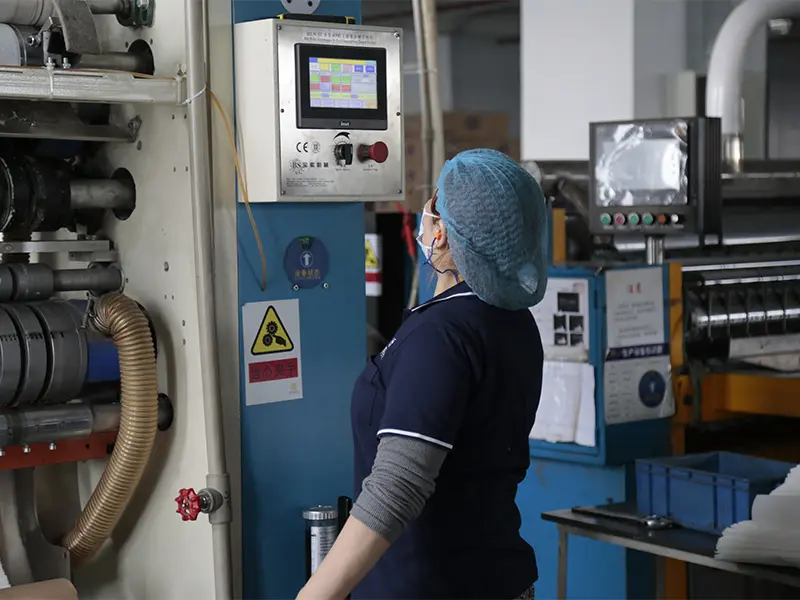
Our high-speed winders, cutters, and packaging machines run with minimal manual intervention, which ensures consistent product specifications and reduces processing defects.
Located near major ocean shipping terminals, we use optimized slip-sheet and pallet-loading patterns that maximize 40HQ container utilization by up to 15%.
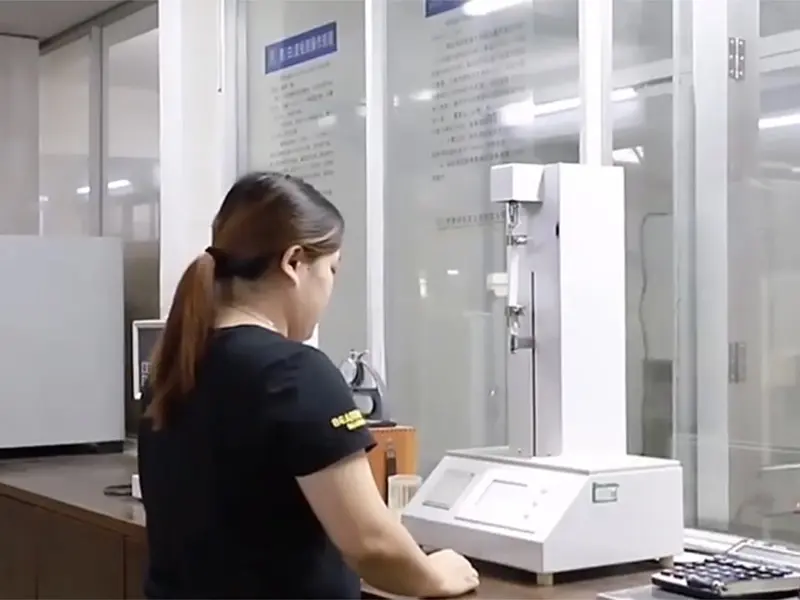
Our production facility operates under strict quality management systems, verified by international certification organizations.
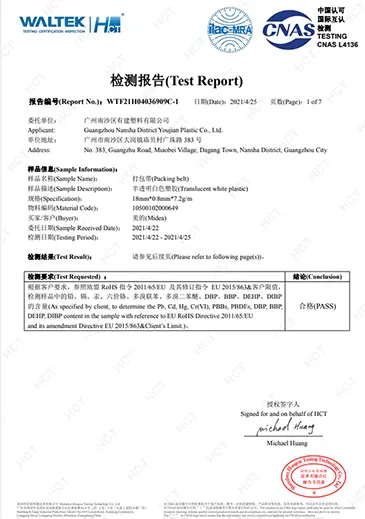
Quality System Audit
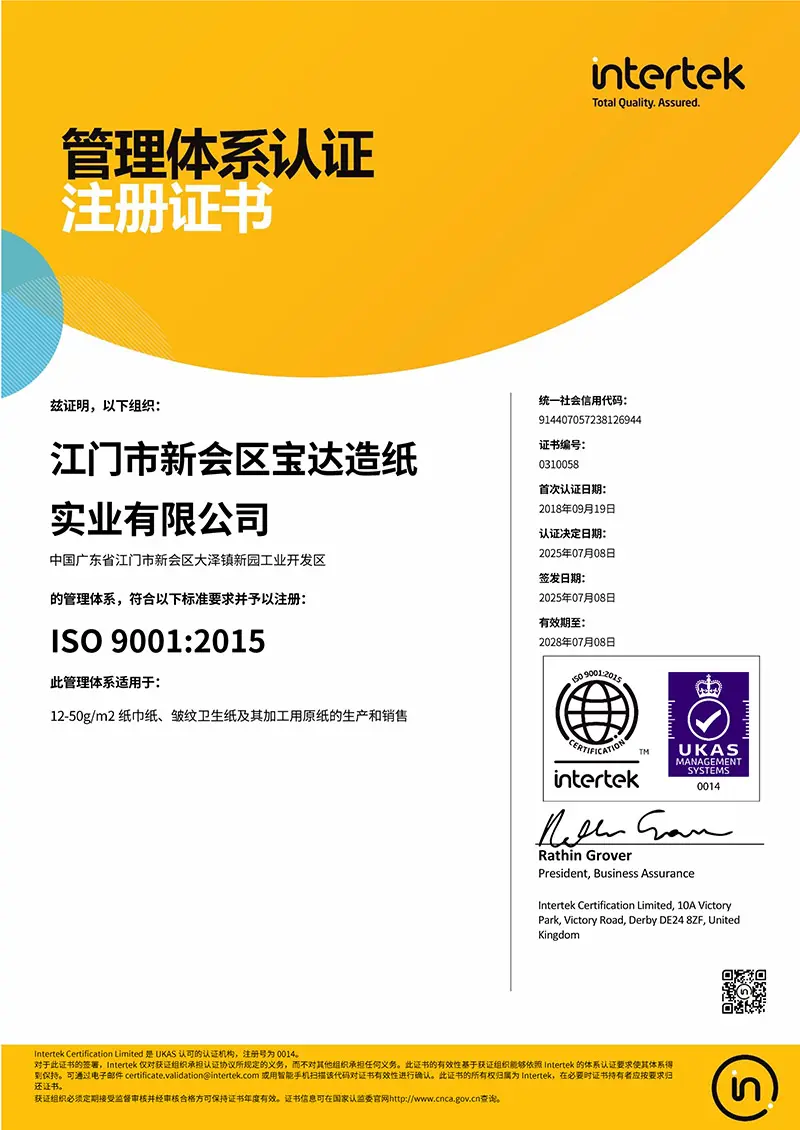
Manufacturing Safety ISO
Raw Materials Conformity
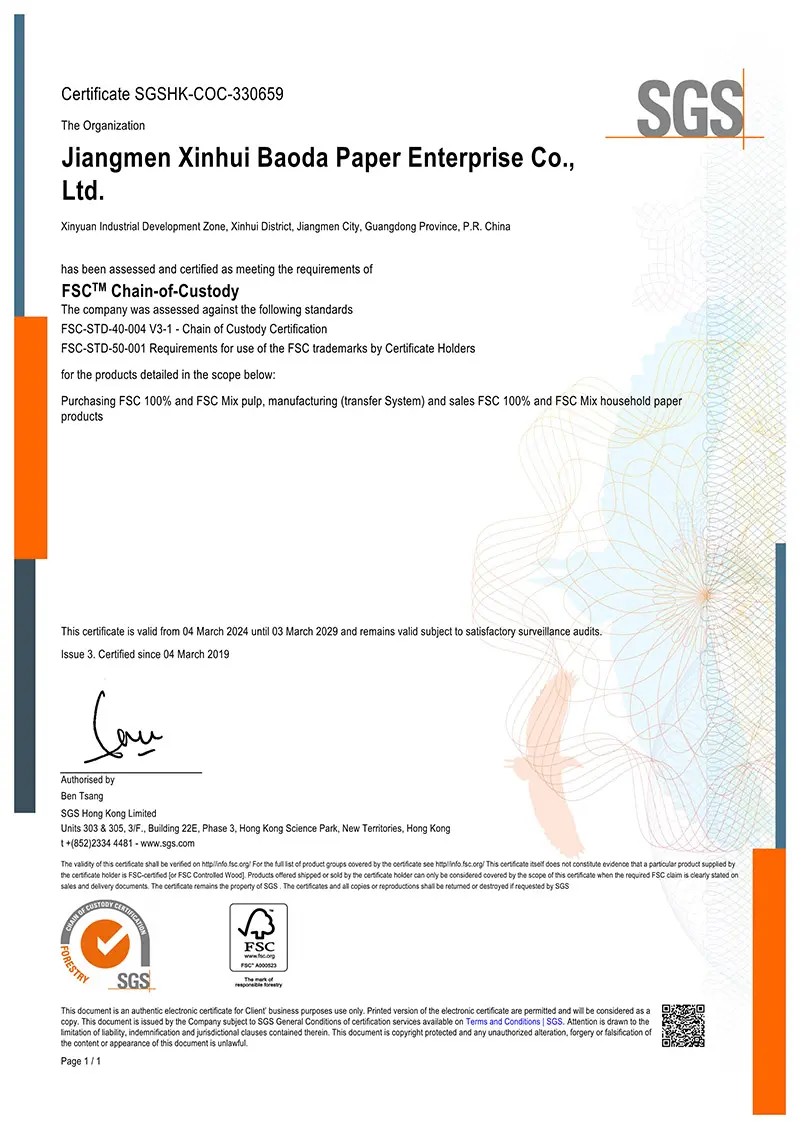
ECO Forestry Traceability
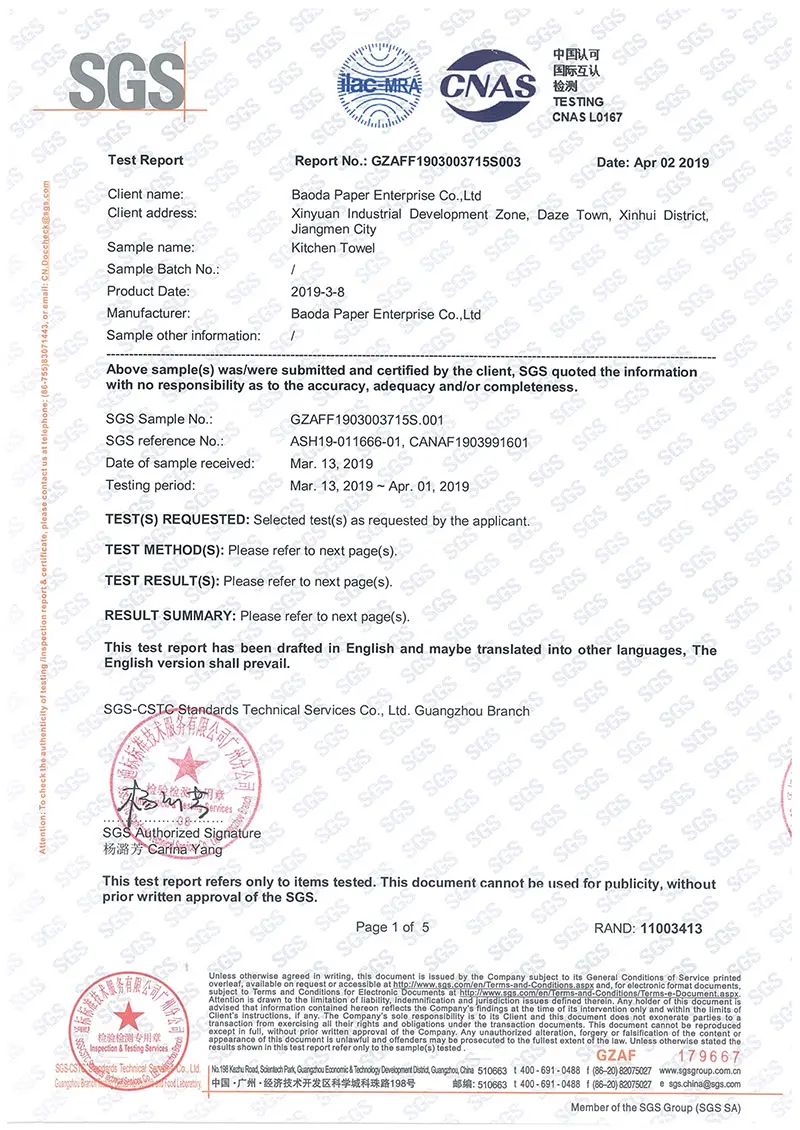
Food Contact Certification
We design tissue products tailored to specific commercial use cases, helping B2B clients offer the right product specifications for their target markets.
Our absorbent, multi-ply napkins and kitchen rolls help restaurants and hotels manage kitchen prep and maintain quick-service hygiene efficiently.
We supply private-label tissue products with shelf-ready packaging, custom barcodes, and consistent roll quality that build customer brand loyalty.
High-capacity hand roll tissue options help commercial buildings minimize maintenance frequency and reduce dispenser refills in high-traffic restrooms.
Answers to common technical, logistics, and compliance questions from procurement managers.
We offer 100% virgin wood pulp, mix pulp, and eco-friendly recycled options. Our virgin wood pulp provides maximum softness and tensile strength, while our recycled options support eco-conscious product positioning.
Our production lines are regularly audited to meet FDA and EU BfR food contact requirements. We do not use elemental chlorine or harmful fluorescent whitening agents (FWA) during the bleaching process, making our towels safe for food prep surfaces.
Our standard Minimum Order Quantity (MOQ) is one 40-foot High Cube (40HQ) container per specification, which optimizes shipping costs. First-time OEM orders typically deliver within 25–30 days, including custom packaging prep. Repeat orders are completed within 15–20 days.
We offer point-to-point and nest-to-nest embossing. These techniques create internal voids between tissue plies, allowing the sheet to trap and hold more oil and water than flat-sheet designs.
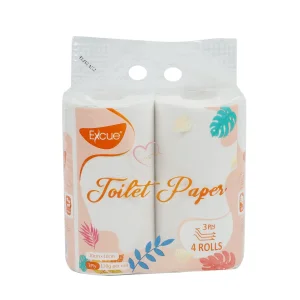
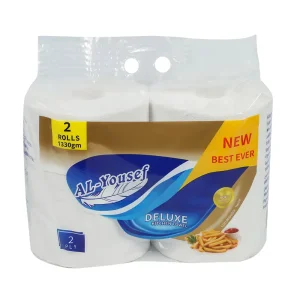
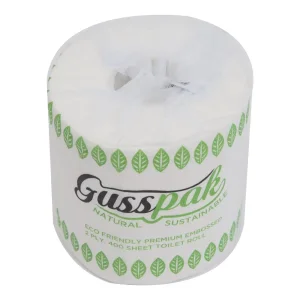
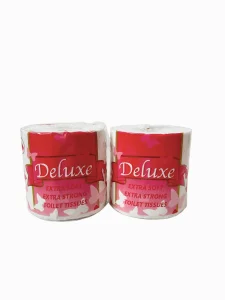
A comprehensive selection of commercial toilet tissue, premium facial napkins, and portable pocket tissues for global distribution.
 BAODA PAPER